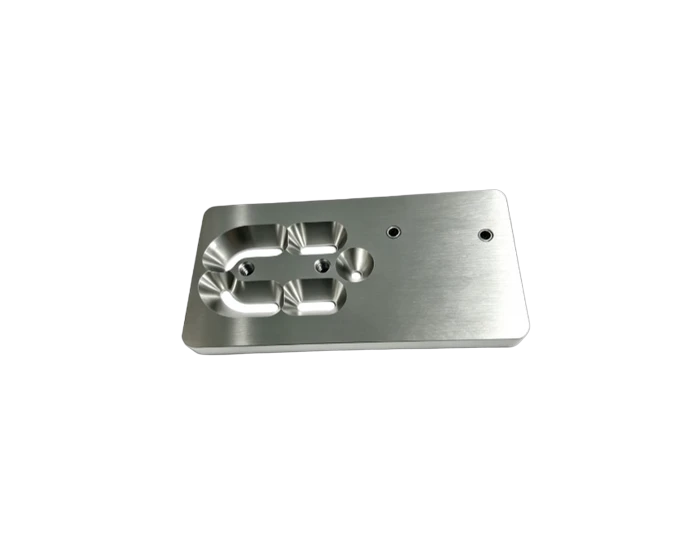
120 x 60 mm Locating Panel in 303 Stainless with Ø4 P7 Dowel Bores
303 stainless locating panel 120 x 60 x 11.8 mm: Ø4 P7 dowel bores at 0.02 mm position, both faces complex milled, go no go gauged 100 percent. Quote in 24 hours, no MOQ.
General Industrial Components
A double sided locating panel with arc counterbores, V angled seats, and through slots on one face, mirrored slot work on the other. The Ø4 P7 dowel bores at 0.02 mm position are the parts that matter.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Stainless steel 303 |
| Process | Face milling and datums, double sided milling of pockets and slots, precision drilling and reaming of P7 bores, laser weld repair and re machining, deburring and cleaning |
| Dimensions | 120 x 60 x 11.8 mm |
| Dowel bores | Ø4 P7 (-0.010/-0.022 mm), position Ø0.02 A|B |
| Threaded holes | 2X N6 and arc counterbore pattern |
| Inspection | Ø3.98 go / Ø3.99 no go plug gauges 100 percent, CMM on datums and positions |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Locating panels earn their keep on the dowel bores. This 120 by 60 by 11.8 mm panel carries Ø4 P7 bores at minus 0.010 to minus 0.022 mm, positioned within 0.02 mm to datums A and B, gauged with Ø3.98 go and Ø3.99 no go plugs on every part, no sampling.
Both faces are heavily milled: arc shaped counterbores, V angled side seats, and threaded holes on one face, with a mirrored pair of long arc through slots on the other. That much removal on a thin 303 plate wants to twist, so clamping force and cutting sequence are staged to keep the panel flat through the process.
One bore carries a laser weld repair and re machining step, which is exactly as interesting as it sounds: weld hardness differs from parent material, so the re machined bore is finish reamed and gauged until the plug gauges confirm the P7 class. The CMM then re verifies datums A, B, C and the dowel positions before release.
This part family supports the Industrial Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Ø4 P7 dowel bores minus 0.010 to minus 0.022 mm, position 0.02 mm
- 100 percent go no go gauging with Ø3.98 / Ø3.99 plugs
- Both faces complex milled: arc pockets, V seats, through slots
- Laser weld repaired bore re machined to P7 and re gauged
- Ground datum faces A, B, C
Typical Applications
- Locating and indexing panels in precision fixtures
- Stainless mounting panels for instrument assemblies
- Position critical interface plates with dowel location
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
| Lead Time | Prototypes 7 to 15 days; production scheduled by volume |
Common Questions
Why 303 and not 304 for a locating panel?
303 machines cleaner and holds small bore finish better, and this panel has no welded assembly around it that would need 304 corrosion performance. For gauged bores, machinability is the point.
What happens to a welded bore?
The weld zone is harder than parent material. The bore is re machined with reduced passes and then gauged 100 percent, because the plug gauge is the only honest verdict on a repaired P7 hole.
More General Industrial Components Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
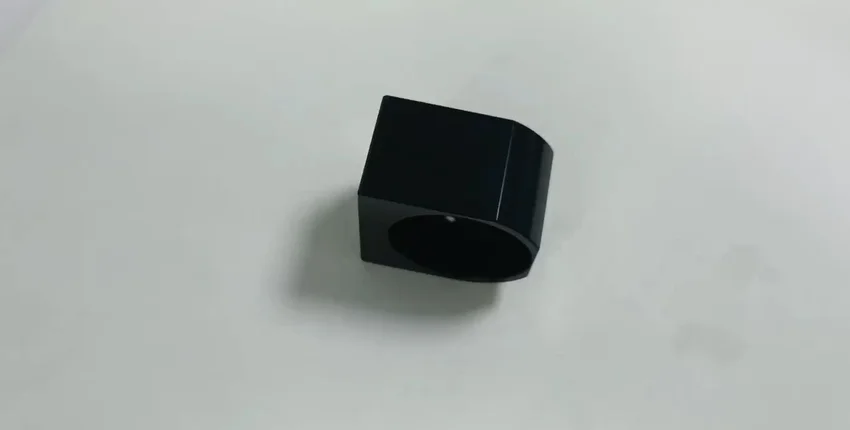
General Industrial Components
CNC Machining Chocolate Equipment Anodized Aluminum Slide Cover
View product →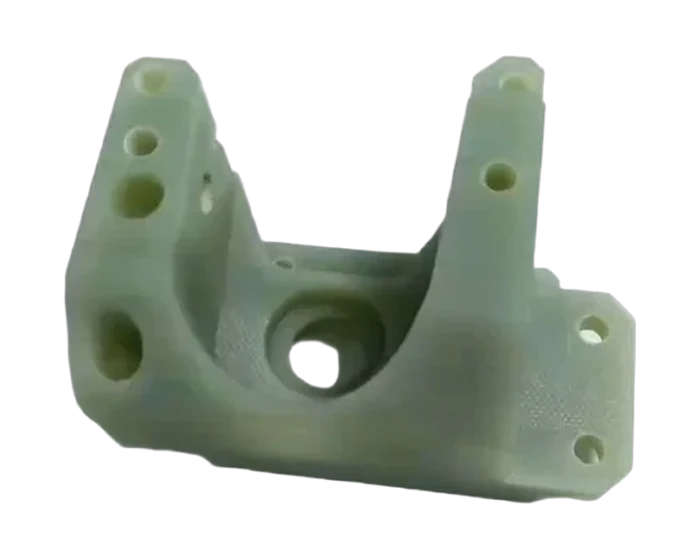
General Industrial Components
CNC Milling Industrial Equipment Filter Nozzle Mounting Base
View product →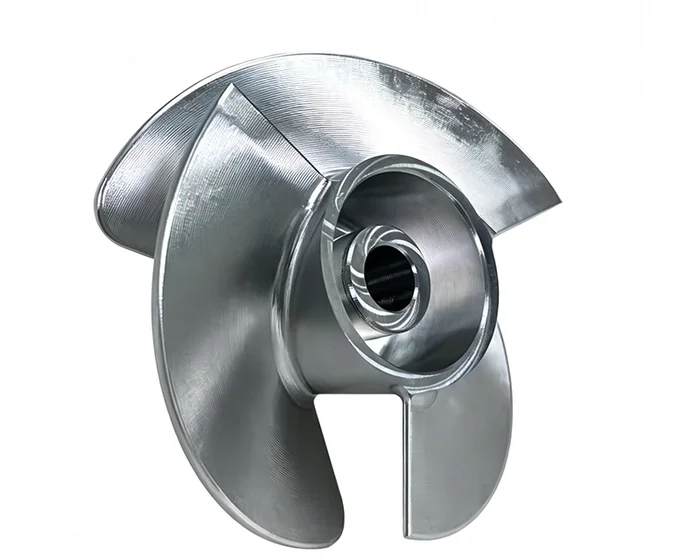
General Industrial Components
For Water SystemsCustom Milling Machining Impeller
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote