Turn-Mill Machining (One-Setup)
Mazak INTEGREX i-250H and i-250HS mill-turn centers complete complex parts in a single setup, reducing handling errors and improving concentricity.
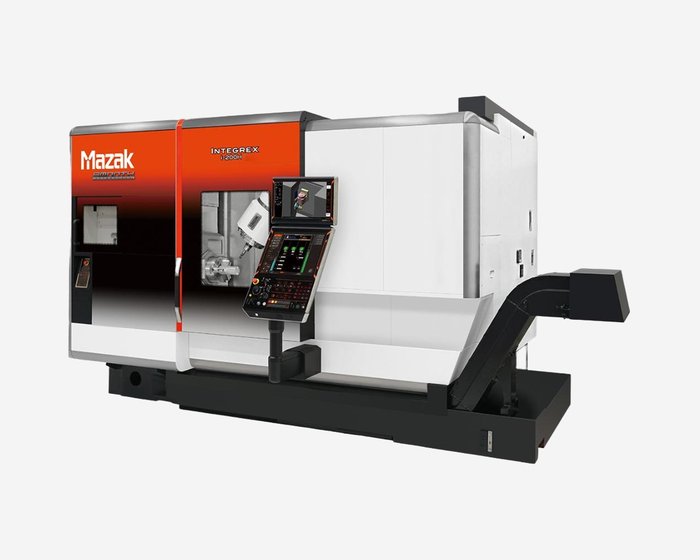
Turn-Mill: One Setup, Complete Parts
The Mazak INTEGREX i-250H and i-250HS are true mill-turn centers that perform turning, milling, drilling, and tapping in one clamping. This eliminates re-fixturing errors and ensures the tightest concentricity between turned and milled features.
When to Specify Turn-Mill
- Parts with turned OD and milled features on the same axis
- Complex shafts with cross-holes, keyways, and flats
- Valve bodies and manifolds
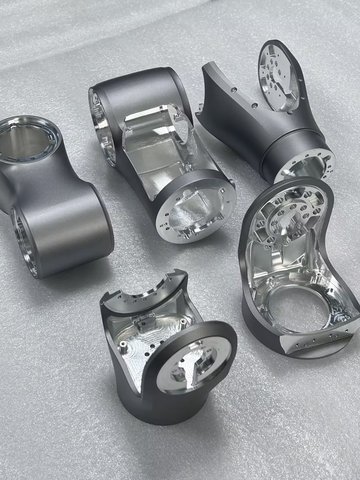
- Robot joint housings
Tolerance
±0.005 mm standard. ±0.002 mm on specific features with full CMM verification.
Sourcing Turn-Mill Parts from Shenzhen
Mill-turn work concentrates machine time into one setup, which is exactly where an offshore piece-price advantage is largest: fewer operations means fewer per-shipment overheads to dilute. If you are weighing a local shop against sourcing directly, our China vs local CNC machining comparison walks through the full total cost of ownership sheet, and the typical turn-mill parts page shows the part families we run. Documentation that ships with every order is listed on the inspection and quality control page.
Frequently Asked Questions
What is the difference between turn-mill and a lathe with live tooling?
Live tooling adds milling moves to a lathe and suits parts with light cross-work. A mill-turn center like the INTEGREX i-250H carries full milling capability (rotating tools with Y-axis and B-axis movement) inside the same machine, so prismatic features, off-center holes, and flats are machined without moving the part to a second machine. The practical difference shows up on parts where the milled content is substantial or positional accuracy between turned and milled features is tight.
What tolerance can turn-mill hold between turned and milled features?
Standard tolerance is ±0.005 mm. On specific features on five-axis mill-turn setups we work to ±0.002 mm with full CMM verification; send the drawing and we confirm which features qualify and what the inspection plan looks like.
Can you quote turn-mill and separate lathe-plus-mill both ways?
Yes. Send the drawing and we price the route that makes sense at your quantity. At low volume a second operation on a separate machine is sometimes cheaper; once milled content or concentricity drives the design, one-setup processing usually wins. The quote states the route we priced and why.
Our Equipment
Machines and representative parts for this capability
| Model / Type | Qty | Notes |
|---|---|---|
| Mazak INTEGREX i-250H / i-250HS | 2 | 5-axis mill-turn |
| CNC turning centers with live tooling | 20 | Shared with CNC turning |
Representative parts machined on this equipment
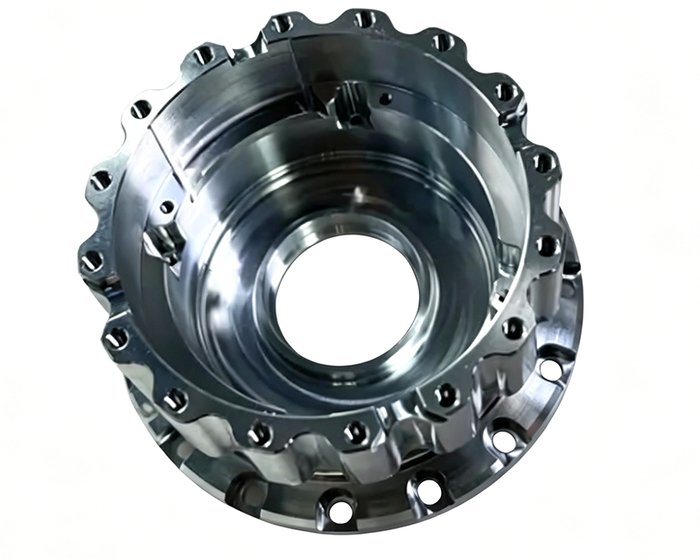
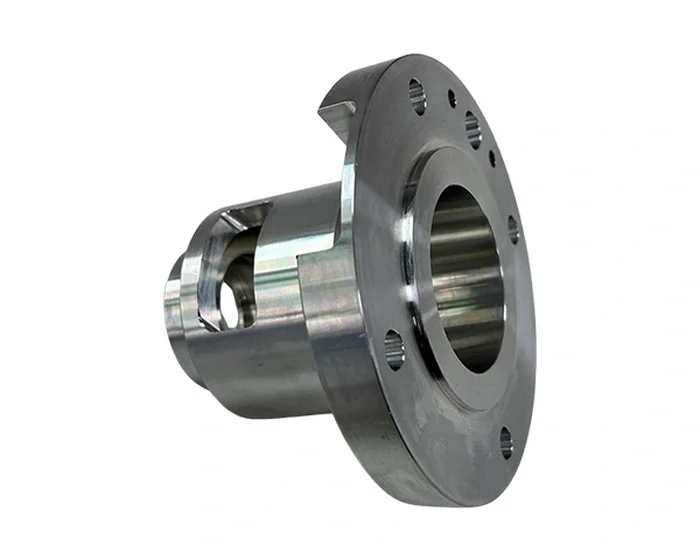
Engineering reference behind this page
The tables and bands the sections above rest on, kept by the same engineering team that runs the work.
- Fits across turned and milled featuresOne part, two processes: how the shared datum carries from the turned body into the milled pockets.
- Process bands side by sideTurning and milling compared, for the features that cross between them.
- Grades that turn and millWhere the same grade behaves differently on the lathe and on the mill.
Full index, including material grades and surface finish data: engineering reference hub.