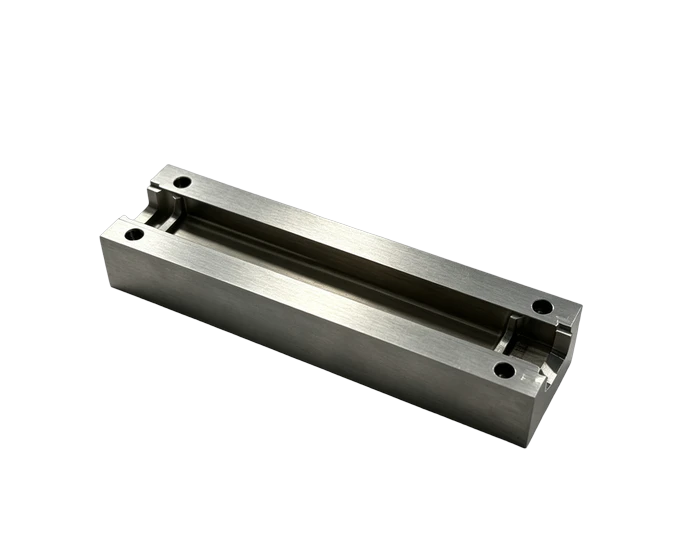
AISI 4140 PH Rear Bridge Insert, Wire EDM and Ground, Plasma Nitrided
AISI 4140 PH rear bridge insert for heated mold assemblies: prehard HRC 28 32, wire EDM rough and finish cuts, plasma nitride surface, inch tolerances to +/-0.0005 in. Quote in 24 hours.
General Industrial Components
A 0.56 lb bridge insert combining CNC milling, wire EDM, and surface grinding. Slot work runs rough fast wire cut plus precision slow wire finish, with two pass milling on the holes.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | AISI 4140 PH, prehard HRC 28-32, plasma nitrided |
| Process | CNC milling, fast and slow wire EDM on slots, surface grinding, two pass hole milling, bench deburring |
| Weight | 0.56 lb |
| Tolerances | fractions +/-1/32, angles +/-0.5 deg, 2 dec +/-0.015 in, 3 dec +/-0.005 in, 4 dec +/-0.0005 in |
| Chamfer | 0.015 x 45 degrees default, all sharp edges removed |
| Inspection | Dimension and visual inspection per drawing |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Heated mold assemblies need inserts that hold geometry through temperature, and this 0.56 lb rear bridge is built for that: AISI 4140 PH in prehard HRC 28 to 32, plasma nitrided for surface wear, with inch drawing tolerances from plus or minus 1/32 on fractions down to plus or minus 0.0005 in on four decimal features.
The slot work is the interesting part. Slots are rough cut on a fast wire EDM, then finish cut on a slow wire pass for the final profile, which splits the heat load and keeps the finish and position where the drawing wants them. Holes are milled in two passes rather than one heavy cut, and the datum faces are surface ground.
The route is honest shop work: mill, bench, fast wire, hand surface grinding, second milling, outside slow wire, CNC mill, deburr, inspect. Blank stock 105.1 by 22.5 by 16.2 mm. Default chamfer 0.015 by 45 degrees with all sharp edges removed.
This part family supports the Industrial Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- AISI 4140 PH prehard HRC 28 32, plasma nitrided
- Slot work: fast wire rough plus slow wire finish EDM
- Inch tolerances to plus or minus 0.0005 in
- Surface ground datums, 0.015 x 45 degree default chamfers
- All sharp edges removed, 0.56 lb finished weight
Typical Applications
- Rear bridge inserts in heated mold assemblies
- Wear inserts in forming and stamping tools
- Precision alloy steel inserts with EDM slot work
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
| Lead Time | Prototypes 7 to 15 days; production scheduled by volume |
Common Questions
Why two EDM passes on the slots?
Roughing dumps heat into the cut and leaves a recast layer. The slow finish pass takes that off and lands the final geometry, so the slot sees one thermal history instead of two.
Why 4140 PH instead of through hardened A2?
Prehard stock means no quench distortion after machining. Plasma nitriding adds surface hardness without moving the core, which is exactly what a geometry critical insert wants.
More General Industrial Components Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
General Industrial Components
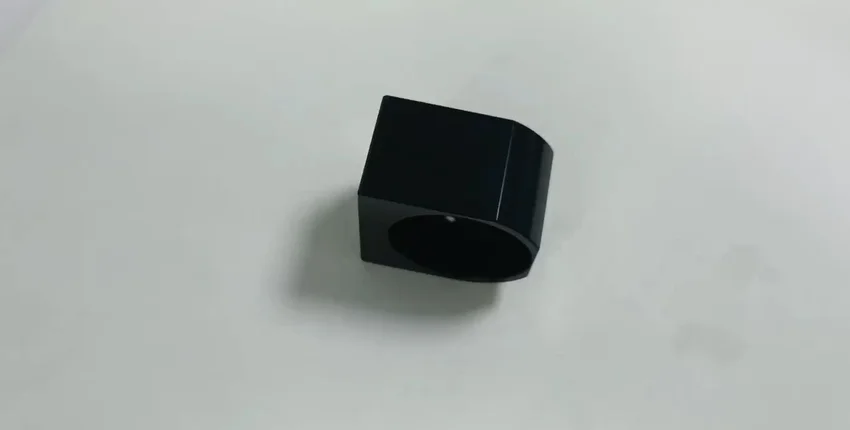
CNC Machining Chocolate Equipment Anodized Aluminum Slide Cover
View product →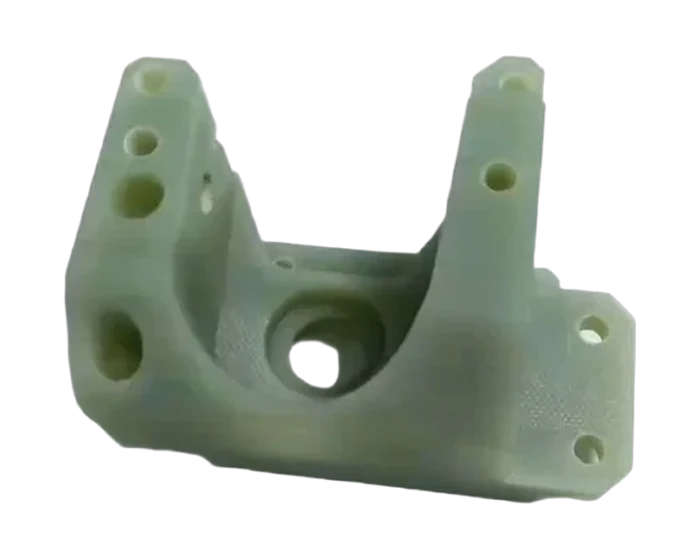
General Industrial Components
CNC Milling Industrial Equipment Filter Nozzle Mounting Base
View product →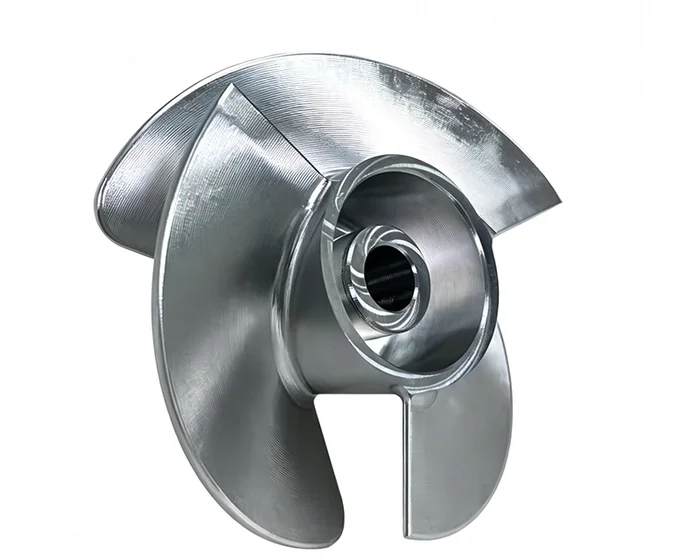
General Industrial Components
For Water SystemsCustom Milling Machining Impeller
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote