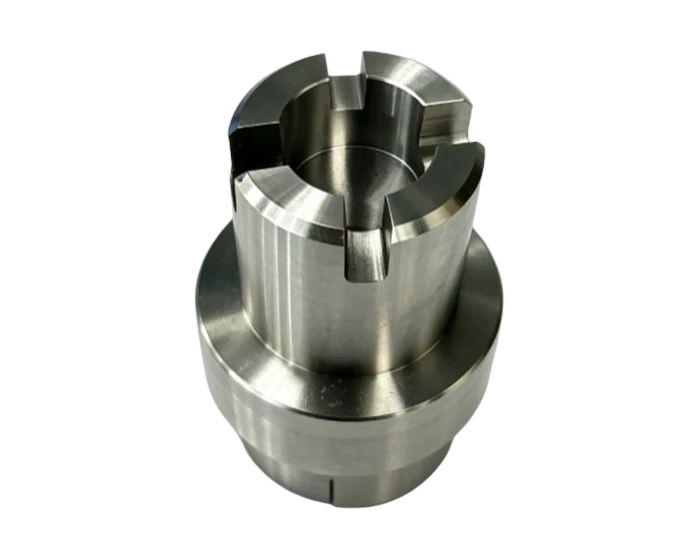
304 Stainless Jaw Clutch Shaft End, CNC Turn Milled
304 stainless jaw clutch shaft end: jaw OD 1.4858 to 1.4870 in, three 120 degree drive jaws, collar 0.8818 to 0.8850 in, passivated, CMM 100 percent. Quote in 24 hours, no MOQ.
General Industrial Components
A turn milled 304 stainless shaft end for jaw clutch drives: stepped bearing diameters, three drive jaws spaced 120 degrees for a spider insert, a precision tail flat slot, 0.02 in chamfers, passivated and gauge checked piece by piece.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Stainless steel S/S 304, bar stock |
| Process | Turn mill turning of stepped diameters, milling of 3X 120 degree jaws and tail slot, side groove milling, micro deburring, passivation |
| Jaw outer diameter | 1.4858 to 1.4870 in (about 37.74 mm) |
| Collar diameter | 0.8818 to 0.8850 in (about 22.48 mm) |
| Jaw pattern | 3X 120 degrees, angular position controlled as a group |
| Chamfers | 0.02 in x 45 degrees on inner and outer edges |
| Surface finish | Up to 32 Ra |
| Inspection | CMM position 100 percent, 3D optical profiler, dedicated go and no go gauges on jaws |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Jaw clutches transmit torque through metal on metal contact, so the jaws take all of it. This shaft end is turned from 304 stainless bar on a turn mill center: the stepped diameters for bearing and collar fits come off the lathe spindle, then the three drive jaws spaced 3X 120 degrees and the tail flat slot are milled in the same setup so the jaw pattern stays true to the axis.
The jaw OD is held between 1.4858 and 1.4870 in (about 37.74 mm) and the collar diameter between 0.8818 and 0.8850 in (about 22.48 mm), tight enough that the spider insert seats without play. Jaw angular position is controlled as a group, because an uneven three jaw pattern shows up immediately as backlash and noise in the drive.
304 work hardens fast, so speeds and feeds are set to keep heat out of the cut and tool wear predictable. Inner corners between jaws are micro deburred by hand to remove the fine flash that would otherwise chew up the insert at high cycle rates. Parts then go through passivation for corrosion resistance and a 100 percent check on a 3D optical profiler and CMM, with go and no go gauges on the jaw form.
This part family supports the Industrial Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Three drive jaws spaced 3X 120 degrees for spider insert coupling
- Jaw OD held 1.4858 to 1.4870 in (about 37.74 mm)
- Collar diameter 0.8818 to 0.8850 in (about 22.48 mm) for axial location
- Precision tail flat slot for keying or lock function
- Turn mill single setup keeps jaw pattern concentric to the shaft axis
- Passivated finish, 3D optical and CMM 100 percent inspection
Typical Applications
- Jaw clutch and jaw coupling shaft ends
- Drive shafts with spider insert torque transmission
- Stepped shafts for industrial power transmission assemblies
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
Why turn mill instead of turning then milling separately?
Reclamping between operations gives up the concentricity between the jaw pattern and the bearing diameters. One setup on the turn mill keeps every feature referred to the same axis, which is what the insert coupling needs.
What is the insert part number you machine to?
The jaws mate with a standard spider insert (PT 17815-00 type). If your clutch uses a different insert, send the jaw print and we will cut to that geometry instead.
Does 304 hold up in wet or washdown environments?
Yes, and the passivation layer helps. 304 is not a seawater grade, but for shop floor and washdown duty with periodic drying it performs well. For constant salt exposure we would quote 316 instead.
More General Industrial Components Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
General Industrial Components
CNC Machining Chocolate Equipment Anodized Aluminum Slide Cover
View product →
General Industrial Components
CNC Milling Industrial Equipment Filter Nozzle Mounting Base
View product →
General Industrial Components
For Water SystemsCustom Milling Machining Impeller
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote