Lead Forming Mold Component in Prehard 4140 PH, Wire EDM and Ground
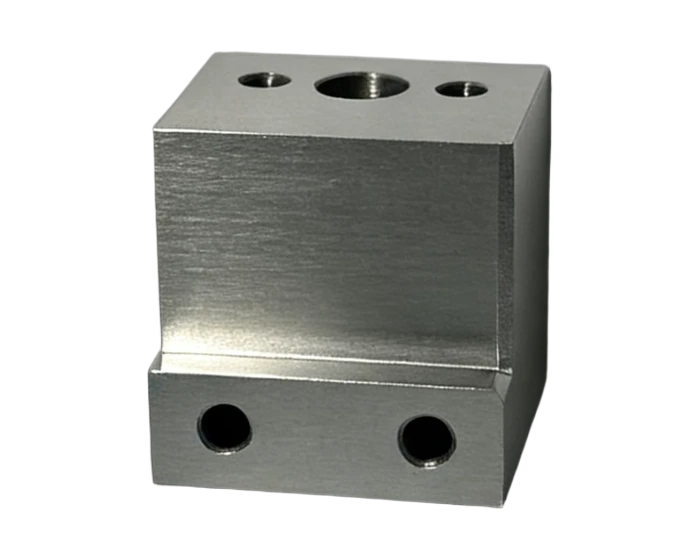
Lead forming mold component in 4140 PH prehard steel: wire EDM profiling, ground six faces, plasma nitrided, inch tolerances to 0.0005, for winding machine forming assemblies. Quote in 24 hours.
General Industrial Components
A lead wire forming mold component for winding machine tooling, cut from 4140 PH prehard steel through wire EDM and precision grinding: six square faces, angled side profiles, plasma nitride wear surface, inch tolerances controlled to the fourth decimal.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | AISI 4140 PH prehard alloy steel, HRC 28-32 |
| Process | Wire EDM rough profiling 0.1 mm stock, surface grinding of six faces and steps, milling of holes, medium speed wire EDM of angled profiles with tool compensation, deburring, plasma nitriding, anti rust oil |
| Tolerances | Fractional +/-1/32, angular +/-1/2 degree, 2 decimals +/-0.015, 3 decimals +/-0.005, 4 decimals +/-0.0005 |
| Surface treatment | Plasma nitride, ground faces |
| Weight | 0.14 lb |
| Hardness check | Material hardness verified before EDM |
| Inspection | Dimensional and appearance check |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Forming molds for lead wire bending see thousands of cycles a day, and the geometry that bends the wire has to survive them. This component is cut from 4140 PH prehard steel at HRC 28 to 32. Wire EDM does the heavy profiling with the outline left 0.1 mm oversize, then a grinding operation squares the six faces and brings the steps to size, which is what gives the mold its true reference faces.
The angled side profiles are cut on a medium speed wire machine with tool compensation passes for finish. Hole features are completed on the mill. The drawing runs inch tolerances: fractional to plus or minus 1/32, two decimals at plus or minus 0.015, three decimals at 0.005, and four decimals at 0.0005, so the EDM and grinding steps carry the precision load while milling handles the rest.
Plasma nitriding after machining hardens the forming surfaces against wear. The part is deburred, dimension and appearance checked, and packed oiled. It drops into the second station forming die assembly of the winding line as a replacement or spare component.
This part family supports the Industrial Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- 4140 PH prehard steel HRC 28-32, stable geometry without heat treatment
- Wire EDM profiling with grinding squared six faces
- Angled side profiles cut with finish passes on medium speed wire
- Inch tolerance control to the fourth decimal place
- Plasma nitride for forming surface wear life
- Replacement component for winding machine forming die assemblies
Typical Applications
- Lead wire forming molds on winding machines
- Forming die insert components in new energy equipment tooling
- Precision wear inserts in metal forming fixtures
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
Why wire EDM instead of milling the profiles?
The forming angles are cut in hardened prehard steel to fourth decimal bands. EDM cuts without cutting force, so the thin form sections do not deflect and the finish is repeatable across replacement batches.
Can you match our existing die assembly?
Send the drawing and, ideally, a mating component or the die station number. The component was built as a station two forming insert and we can cut to your revision geometry.
How long does the nitrided surface last?
Nitriding adds a hard diffusion layer that resists abrasive wear from the wire. Actual life depends on wire material and cycle rate; in comparable winding tooling the nitrided faces typically run several times longer than bare machined steel.
More General Industrial Components Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
General Industrial Components
CNC Machining Chocolate Equipment Anodized Aluminum Slide Cover
View product →
General Industrial Components
CNC Milling Industrial Equipment Filter Nozzle Mounting Base
View product →
General Industrial Components
For Water SystemsCustom Milling Machining Impeller
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote