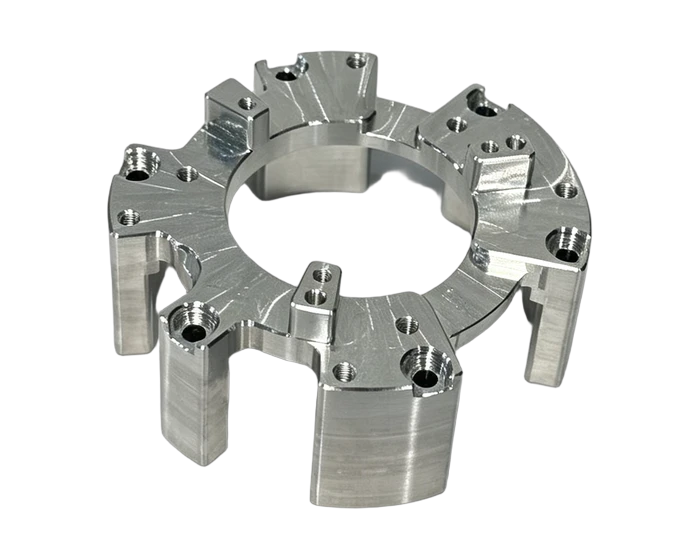
14S Servo Brake Mounting Seat in 6061-T6 Aluminum, CNC Milled
6061-T6 extruded servo brake mount for 14S frame motors: two setup interchangeable fixture machining, 3X M2.5 milled threads, burr free bare aluminum, RoHS 2.0. Quote in 24 hours, no MOQ.
Robotics & Humanoid Robots
A compact brake mounting seat machined from 6061-T6 extrusion for 14S frame servo and humanoid robot motors: two setup machining on interchangeable fixtures, in machine milled M2.5 threads, deburred by hand, shipped bare with RoHS 2.0 compliance.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | 6061-T6 aluminum extrusion, die JW-1077-002-01 |
| Process | CNC milling op 1 on B datum (bore, outline, 3X M2.5 milled threads), op 2 on interchangeable fixture for reverse features, hand deburring, inspection, cleaning, packing |
| Weight | 0.04 kg per piece |
| Edge defaults | R0.3 radii, C0.3 chamfers where unspecified |
| Surface | No finish, bare machined aluminum |
| Compliance | RoHS 2.0 |
| Inspection | Dimensional check plus visual appearance check on every piece |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Brake seats are production parts, and this one is set up to run that way. The blank is 6061-T6 extrusion from die JW-1077-002-01, machined in two CNC operations on a pair of interchangeable fixtures so front and back features stay referenced to the same datums. B face bore, outline, and three M2.5 threads are cut in the first op, the reverse features in the second, with the threads milled in machine rather than tapped for cleaner form control.
The part is small at 0.04 kg with compact radii, R0.3 and C0.3 default, so edge condition matters more than usual: after machining every piece goes through hand deburring and visual inspection before cleaning and packing. No surface treatment, the bare aluminum ships as machined, and the finished part meets RoHS 2.0.
First angle projection drawing in metric, checked piece by piece on dimensions and appearance. The same route scales from prototype batches to the running production volumes this seat was designed for.
This part family supports the Robotics Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- 6061-T6 extrusion stock, die code JW-1077-002-01, for stable supply
- Two setup machining on interchangeable fixtures for datum consistency
- 3X M2.5 threads milled in machine for clean thread form
- Compact 0.04 kg part with R0.3 and C0.3 default edge control
- Hand deburred, burr and flash free before packing
- Bare machined aluminum, RoHS 2.0 compliant for overseas motor customers
Typical Applications
- Brake mounting seats on 14S frame servo motors
- Brake structure parts in humanoid robot actuators
- Compact motor accessory mounts in automation equipment
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
Why machine from extrusion instead of plate?
The extrusion profile matches the seat geometry, so less material becomes chips and the grain structure follows the part. It also locks in supply: the die is registered and stock is repeatable batch to batch.
Why mill the M2.5 threads instead of tapping?
In machine thread milling leaves a cleaner, rounder thread in 6061 and eliminates tap breakage risk in small holes. For a part that runs in volume, that reliability is worth the cycle time.
Do you support the bare finish for outdoor or wet use?
Bare 6061 forms its own oxide layer and does fine indoors and in enclosures. For wet or outdoor duty we would quote clear anodize on the same route.
More Robotics & Humanoid Robots Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote