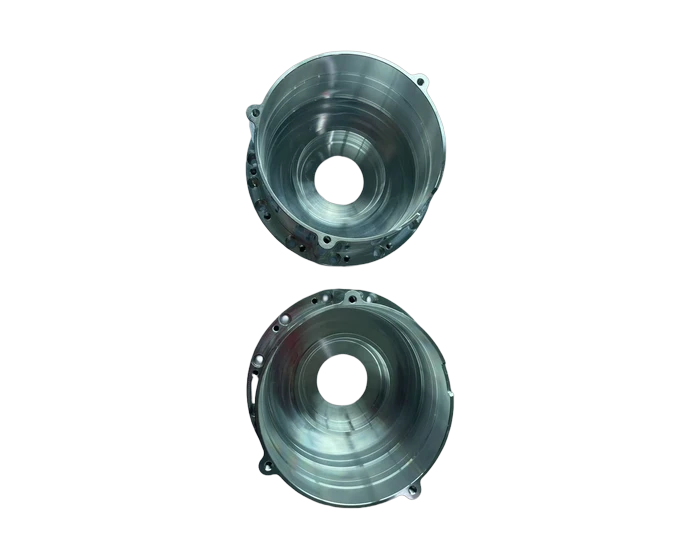
6061-T6 Motor Housing, Ø95 H7 / Ø55 H6 Bores, CMM Verified
6061-T6 cylindrical motor housing: Ø95 H7 and Ø55 H6 bearing bores, 3-M4 and Ø6.5 through holes, geometric tolerance 0.02 mm, as machined finish, RoHS 2.0. Quote in 24 hours.
Robotics & Humanoid Robots
A cylindrical motor housing milled and turned from 6061-T6: multi step bearing bores at Ø95 H7, Ø55 H6, and Ø66 h6, 3-M4 and Ø6.5 through holes, geometric tolerances at 0.02 mm, delivered in as machined finish at 0.28 kg.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Aluminum 6061-T6 (ASTM B221), tensile ≥290 MPa, yield ≥240 MPa |
| Process | CNC vertical and horizontal milling of flange and internal steps; turning of OD and bores; drilling 3-M4 and Ø6.5 through holes; fine boring of Ø95 H7 and Ø55 H6; deburring |
| Bearing bores | Ø95 H7 (+0.04/0 mm); Ø55 H6 (+0.02/0 mm); Ø66 h6 |
| External features | OD Ø99; max flange Ø92.5; Ø93.95 +0.05/0; Ø93.75 G6 |
| Geometric tolerances | Perpendicularity, parallelism, and position ≤0.02 mm |
| Surface finish | Ra 1.6 turned faces; Ra 0.8 sealing faces |
| Unit weight | 0.28 kg |
| Finish | As machined, no surface treatment, RoHS 2.0 |
| Inspection | CMM full check of bores and geometric tolerances; thread gauges |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
This housing wraps a 25 frame motor with a set of concentric, multi step bearing bores that decide how smoothly the rotor spins: Ø95 H7, Ø55 H6, and Ø66 h6, each machined to run true to the next. The flange and internal steps are milled on vertical and horizontal centers, then the external diameter and bores are turned, keeping every concentric feature off one setup family.
Mounting comes from three M4 through holes and a Ø6.5 through hole, positioned against geometric controls of 0.02 mm for perpendicularity, parallelism, and position. Fitted faces finish at Ra 1.6 with sealing faces at Ra 0.8.
The part ships in as machined 6061-T6 with no coating, which suits RoHS 2.0 requirements and keeps the housing dimensionally exact. CMM checks the bores and geometric tolerances on every lot, with thread gauges closing out the tapped holes.
This part family supports the Robotics Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Three concentric bearing bores: Ø95 H7, Ø55 H6, and Ø66 h6
- Geometric controls at 0.02 mm on perpendicularity, parallelism, and position
- 3-M4 through holes plus Ø6.5 through hole per the drawing
- Ra 1.6 on turned faces, Ra 0.8 on sealing faces
- As machined 6061-T6 finish, no coating, RoHS 2.0 compliant
- Light at 0.28 kg with T6 strength (tensile ≥290 MPa, yield ≥240 MPa)
Typical Applications
- Housings for servo and stepper motors in 25 frame class
- Motor mounts and seats on automation equipment
- Housings for precision reducers and gearboxes
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
Why as machined with no anodize?
The customer drawing specified it: as machined 6061-T6 keeps every dimension exact with no film growth, suits RoHS requirements, and lets the end user coat it their way. Anodizing is available as a quote option.
Can you hold H6 on an aluminum bore in volume?
Yes. The bore is fine bored after the external turning is complete, with thermal soak and in-process plug gauging, and CMM verifies every lot.
Is this housing limited to a 25 frame motor?
No, the dimensions come from one delivered design. Send your frame drawing and we will quote the same route to your numbers.
More Robotics & Humanoid Robots Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote