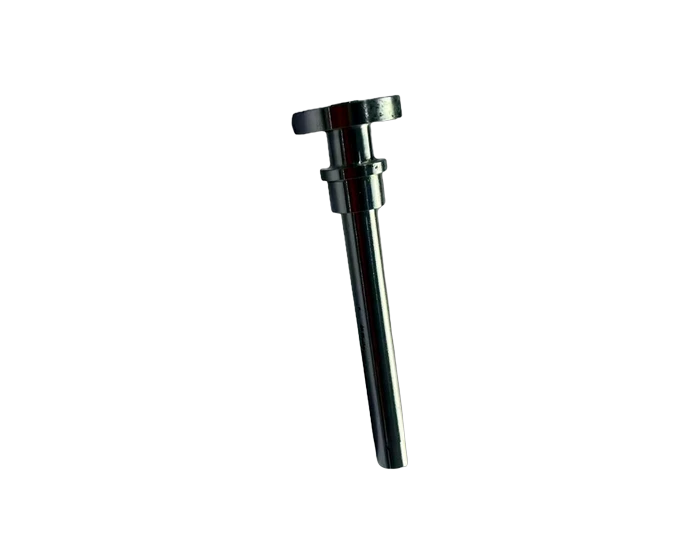
Encoder Shaft Seat in 7075-T6, Ø6.5 g6 Shaft and h7 Seats
7075-T6 encoder shaft seat: Ø6.5 g6 shaft, Ø10 and Ø5 h7 seats, 2X Ø2 H7 and 2X M2 radial features, end runout 0.01 A, 180 grit blast and black anodize. Quote in 24 hours.
Robotics & Humanoid Robots
A 71.5 mm stepped encoder shaft seat for servo and automation drives, with multiple g6 and h7 journal classes on one axis and a controlled end face runout.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Aluminum 7075-T6 |
| Process | CNC turning of journals and steps, drill and ream of radial H7 bores, M2 tapping, deburring, 180 grit blast, black anodize |
| Journals | Ø6.5 g6 (+0.005/+0.013), Ø10 h7 (-0.02), Ø5 h7 (-0.01) |
| Lengths | 71.5 +/-0.2 overall, 58.75 +/-0.05, 12.2 +/-0.02 |
| Radial features | 2X Ø2 H7 (+0.01) 3 deep, 2X M2 6 deep |
| Runout | 0.01 A end face |
| Inspection | Micrometer and caliper, CMM on runout and coaxiality, thread gauges, appearance |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Encoder mounts are journal stacks, and this seat runs them on one axis: Ø6.5 g6 shaft at +0.005/+0.013, Ø10 h7 at minus 0.02, Ø5 h7 at minus 0.01, over a 71.5 plus or minus 0.2 mm length with controlled steps at 58.75 plus or minus 0.05 and 12.2 plus or minus 0.02. End face runout is held at 0.01 A.
Radial features carry the encoder hardware: 2X Ø2 H7 bores 3 mm deep and 2X M2 threads 6 mm deep. The finish is 180 grit bead blast plus black anodize, with the journal classes protected or finished after treatment.
Inspection is micrometer and caliper, CMM on runout and coaxiality, thread gauges, and appearance.
This part family supports the Robotics Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Ø6.5 g6, Ø10 h7, and Ø5 h7 journals on one axis
- End face runout 0.01 A
- 2X Ø2 H7 bores and 2X M2 threads, radial
- 58.75 +/-0.05 and 12.2 +/-0.02 controlled steps
- 180 grit blast plus black anodize, journals protected
Typical Applications
- Encoder shaft seats for servo motors
- Positioning shafts in precision automation
- Servo output shaft companion seats
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
| Lead Time | Prototypes 7 to 15 days; production scheduled by volume |
Common Questions
Why so many journal classes on one shaft?
Each mating part gets the class it needs: the encoder, the bearing, the coupling. One axis, three classes, all verified on the CMM together.
Does the anodize move the g6 journal?
It would if ignored. Journal diameters are masked or finished after treatment so the class ships as drawn.
More Robotics & Humanoid Robots Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote