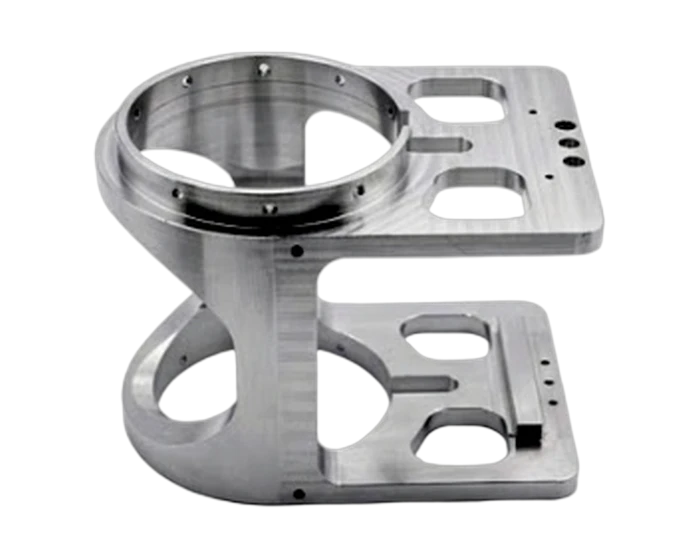
Dual-Column Joint Frame in 7075-T6, Five-Axis Machined
Five-axis machined dual-column joint frame in 7075-T6/6061-T6: bearing stops coaxial within 0.008 mm, H6/H7 fits, arc windows for weight relief, 100 percent burr free. Quote in 24 hours.
Robotics & Humanoid Robots
A monolithic dual-column joint frame milled from 7075-T6 or 6061-T6 billet: two large bearing stops coaxial within 0.008 mm, end face runout within 0.005 mm, H6/H7 fits, and arc shaped weight relief windows, all CMM verified.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | High strength aerospace aluminum 7075-T6 / 6061-T6 (ASTM B221) |
| Process | 5-axis simultaneous milling in one or two setups; precision finishing of twin bearing stops; arc window and pocket milling; drilling and tapping; ultrasonic cleaning; micro deburring; CMM inspection |
| Bearing stop coaxiality | ≤0.008 mm; end face runout ≤0.005 mm |
| Fitting faces | H6 / H7, about ±0.005 mm |
| Parallelism | ≤0.01 mm per meter on inner column faces and end faces |
| Surface finish | Ra 0.4 to 0.8 um in bearing chambers and stops; clean as-milled outside |
| Edge condition | Micro chamfers on crossover holes and window corners, 100 percent burr free |
| Inspection | CMM on stop coaxiality, span, and positions; air gauge or bore micrometer on bearing chambers; thread gauges |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
This frame is the load path of a robot shoulder, elbow, hip, or torso joint, so it is milled from one billet with no welds to flex or crack. The two columns carry large diameter bearing stops on opposite faces, and five-axis machining aligns those stops to each other: coaxiality within 0.008 mm and end face runout within 0.005 mm, which is what keeps the joint smooth and free of backlash under dynamic load.
Bearing seats and fitting faces are held at H6/H7 (about ±0.005 mm) and finished to Ra 0.4 to 0.8 um. Between the columns, large arc shaped windows and deep pockets strip out every gram of dead weight while the remaining ribs keep torsional stiffness high, and the inner column faces stay parallel within 0.01 mm per meter.
Every crossover hole and window corner is micro chamfered, and the frame leaves the line 100 percent free of burrs and sharp edges. CMM measures the two stops, the span, and the hole positions on every lot, with air gauges or bore micrometers confirming the bearing seats.
This part family supports the Robotics Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Monolithic billet construction, no welds, maximum torsional and bending stiffness
- Twin bearing stops coaxial within 0.008 mm, end faces within 0.005 mm runout
- H6/H7 fitting faces (about ±0.005 mm) at Ra 0.4 to 0.8 um
- Large arc windows and deep pockets cut mass while keeping the load path intact
- Inner column faces parallel within 0.01 mm/m
- 100 percent burr free with micro chamfers on every crossover hole and corner
Typical Applications
- Shoulder, elbow, hip, and torso support frames for humanoid robots
- Second and third joint housings and reducer mounts for collaborative arms
- High dynamic rotary and swing mechanism bases on precision equipment
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
Why a monolithic frame instead of a welded assembly?
A single billet has no weld seams, so there is nothing to distort under heat or fatigue around. For a joint frame that swings thousands of cycles a day, the one piece route pays for itself in kept alignment.
How do you keep both bearing stops aligned across such a span?
Both stops are finished in the same five-axis setup referencing one datum, with thermal soak and in-process gauging. CMM then measures stop to stop coaxiality directly, and the report ships with the parts.
Can the window pattern follow my topology study?
Yes. Send the STEP with your window geometry and we will quote it as drawn, or propose a near equivalent that is cheaper to machine while keeping the stiffness targets.
More Robotics & Humanoid Robots Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote