Robot Joint Shell Housing in 6061-T6, Turned and 5 Axis Milled, Black Anodized
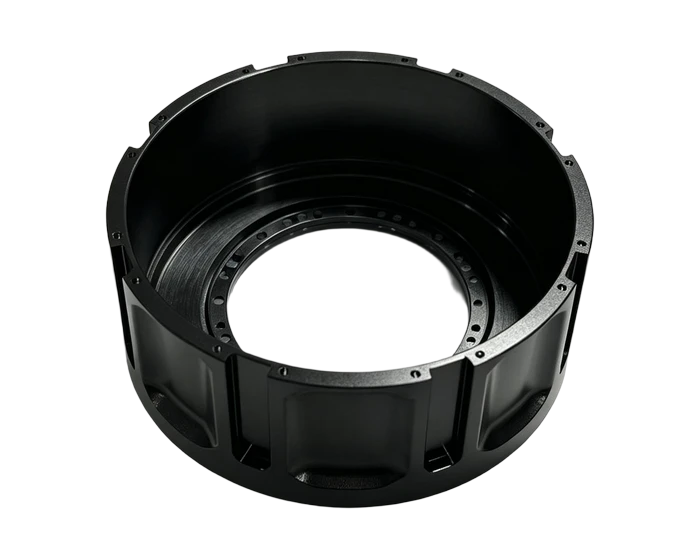
Robot joint shell from 6061-T6 tube: turning plus 4 and 5 axis milling, stress relieved at 180 C, black anodized 10 to 15 um with pre anodize size compensation, laser marked. Quote in 24 hours.
Robotics & Humanoid Robots
A humanoid robot joint shell machined from 6061-T6 tube through turning, 4 axis, and 5 axis operations with an 180 C stress relief in the middle of the route, then black anodized at 10 to 15 um with size compensation so fits hold after coating.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | 6061-T6 aluminum tube, blank 100 to 50 x 41 mm section |
| Process | Turning rough, stress relief 180 C x 4 h furnace cool, 4 axis milling, finish turning of A datum faces and 52.5 mm bore, 5 axis side holes, milling reverse holes, deburring, black anodizing, laser marking |
| Tolerance class | GB/T 1804-m dimensions, GB/T 1184-K form |
| Anodize | Black, film thickness 10 to 15 um, hung not clamped |
| Size compensation | 0.005 mm per side under size on critical fits before coating |
| Weight | 91.9 g per piece |
| Marking | Laser marked with supplier, production date, part number |
| Inspection | In process dimensional, CMM, post anodize dimensional and marking recheck |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Joint shells wrap motors and sensors in humanoid robots, and they get machined, not cast, when the fits matter. This shell starts as 6061-T6 tube at 100 by 50 mm section. Turning opens the rotating diameters with stock left, and the part then goes through a 180 C four hour aging cycle with furnace cooling to pull residual stress out before the walls get thin.
After stress relief, a 4 axis op machines the side slots and pockets, then finish turning cuts the A datum faces and the 52.5 mm bore in one pass, followed by 5 axis work on the side hole pattern. Every critical fit dimension is cut 0.005 mm per side under size, because the 10 to 15 um black anodize builds up on the surface and the coating growth has to land inside tolerance, not on top of it.
Anodizing runs with hanging fixtures, never squeeze clamping, to avoid marks on the finished faces. After coating, dimensions and appearance are rechecked, then the shell is laser marked with supplier, date, and part number for traceability. The result is a light, stable, scratch resistant joint housing that assembles without post machining.
This part family supports the Robotics Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Turned from 6061-T6 tube, light and dimensionally stable
- 180 C four hour stress relief between roughing and finishing
- A datum bore 52.5 mm cut in one pass at finish turning
- 4 axis plus 5 axis milling for side slots, pockets, and hole pattern
- Pre anodize size compensation of 0.005 mm per side on critical fits
- Black anodize 10 to 15 um, laser traceability marking
Typical Applications
- Joint housings for humanoid robot arms and legs
- Rotary actuator shells in robotics and automation
- Protected sensor and motor enclosures in precision mechanisms
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
Why stress relieve in the middle of the route?
Because the walls are still thick when the big cuts happen. Aging at 180 C after roughing releases the locked in stress before finish turning and 5 axis work, so the thin walls stay true instead of springing after machining.
How does the coating end up in tolerance?
We machine critical fits 0.005 mm per side under size. Anodize builds about 10 to 15 um on the surface, the growth lands on the deliberately small dimensions, and post coating checks confirm the final size.
Can the marking content be our part numbers?
Yes. Laser marking content is set per drawing, including your part number, date code, and any RoHS or traceability text you require.
More Robotics & Humanoid Robots Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote