Micro Drive Module End Effector, 5-Axis Machined 6061-T6
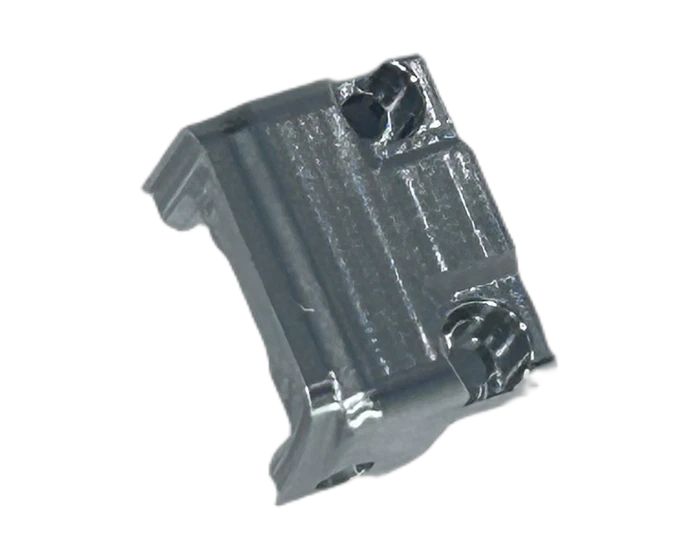
CNC machined micro drive module end effector in 6061-T6: thin-wall asymmetric cavities, micro threads, fitting steps at ±0.01 mm, CMM verified. Quote within 24 hours.
Robotics & Humanoid Robots
KGL machines micro drive module end effectors from 6061-T6 aluminum: asymmetric thin-wall cavities, multi-face micro threads and counterbores, fitting steps held at ±0.01 mm, and every critical feature CMM verified before shipment.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Aluminum 6061-T6 (ASTM B221) |
| Process | 5-axis milling with turn-mill support; cavity and thin-wall precision milling; micro drilling and tapping; ultrasonic cleaning; micro deburring; CMM inspection |
| General tolerance | GB/T 1804-m (about ±0.05 to ±0.10 mm) |
| Fitting steps and slots | ±0.01 mm |
| Surface finish | Ra 0.8 um on fitting faces and cavity walls |
| Threads and holes | Precision tapped, full form, no collapsed entries; counterbores chamfered smooth |
| Edge condition | All edges broken to C0.1 to C0.2, free of burrs and nicks |
| Inspection | CMM on key bores, steps, and positions; thread gauges; stereo microscope for micro burrs |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
This end effector is the structural core of a compact drive module: a single 6061-T6 block that carries motor mounts, sensor bosses, and routing passages in a body small enough to sit inside a dexterous hand. The geometry is deliberately asymmetric, with thin walls and deep stepped cavities milled to cut every gram that the drawing does not need while keeping the frame stiff under load.
We rough and finish the part in five-axis clamping, so the cavity floors, side walls, micro tapped holes, and counterbored mounting faces all stay referenced to one datum system. Fitting steps and slots are held at ±0.01 mm, general features follow GB/T 1804-m, and internal corners come off the cutter smooth, without the tool marks that scratch mating parts during assembly.
After machining, parts are ultrasonic cleaned and micro deburred, then every critical bore, step, and position is verified on CMM. Thread gauges confirm each tapped hole, and a stereo microscope check catches burrs smaller than the eye can see before the part is packed.
This part family supports the Robotics Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Asymmetric thin-wall cavity design milled from solid 6061-T6 for maximum stiffness at minimum mass
- Fitting steps and slots held at ±0.01 mm, general features to GB/T 1804-m
- Multi-face micro threads, counterbores, and locating slots finished in one datum system
- Smooth internal corners and cavity walls free of cutter marks for clean assembly
- All edges broken to C0.1 to C0.2 with micro deburring under magnification
- CMM inspection of every critical bore, step, and position before packing
Typical Applications
- Dexterous hand and micro actuator frames for humanoid robots
- Precision micro drive pumps for medical and biological instruments
- Mounting frames for high sensitivity optical sensors
- Structural bases for compact automation modules and micro linear drives
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
Why 6061-T6 for a micro drive module body?
6061-T6 gives a strong stiffness to weight ratio, machines cleanly at small feature sizes, and anodizes well for corrosion protection. For a part that lives inside a compact actuator, that balance of strength, mass, and machinability beats most alternatives.
How do you hold ±0.01 mm on internal steps at this size?
The cavities and steps are finished in five-axis clamping so every feature shares one datum system, with no re-fixture error. Thermal soak, sharp tooling, and in-process gauging keep the cuts inside the band, and CMM confirms the result feature by feature.
Can you quote from a 3D model alone?
Yes. Send STEP plus a drawing where tolerances matter, and we return DFM feedback and a quotation within 24 hours. One-piece prototypes carry no minimum order.
More Robotics & Humanoid Robots Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote