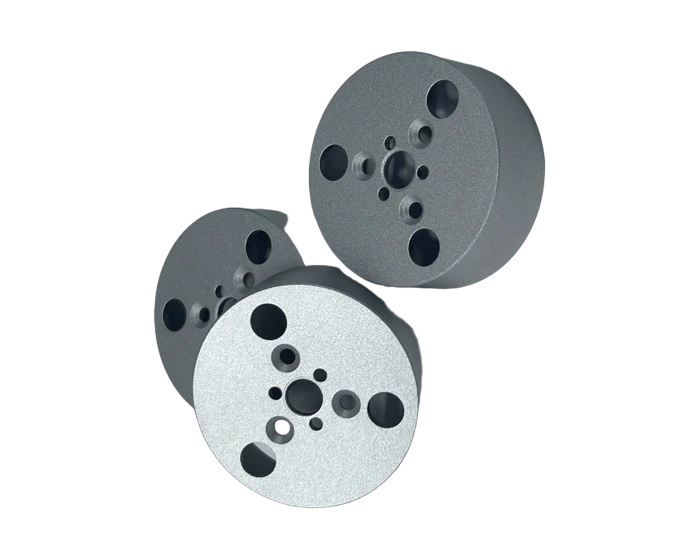
Perforated Cylinder End Cap, 6061/7075 with Silver Anodize
CNC machined perforated cylinder end cap in 6061-T6 or 7075-T6: coaxiality 0.015 mm, hole position 0.02 mm, Ra 0.8 fits, bead blasted silver anodize 8 to 15 um. Quote in 24 hours.
Robotics & Humanoid Robots
A thin wall cylinder end cap turned and machined from 6061-T6 or 7075-T6, with bore coaxiality within 0.015 mm, hole pattern position within 0.02 mm, and an even bead blasted silver anodized finish for robot joint and motor housings.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Aluminum 6061-T6 or 7075-T6 (ASTM B221) |
| Process | CNC turning of OD, bore, and faces; machining center drilling, counterboring, and tapping; micro deburring; bead blasting; silver anodizing; laser marking; CMM inspection |
| Fitted diameters | IT6 to IT7 (H7/f7 class, about ±0.01 mm) |
| Coaxiality | ≤0.015 mm; runout ≤0.01 mm |
| Hole pattern | Position ≤0.02 mm on tapped and through holes |
| Surface finish | Ra 0.8 um on fitting faces and bore; even bead blast outside |
| Anodize film | 8 to 15 um, silver |
| Inspection | CMM on bore coaxiality and hole positions; micrometer; thread gauges; roughness tester |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Joint and motor housings live or die by how true their end caps run. This cap is turned from aluminum bar on a CNC lathe, then moved to a machining center for the bolt circle, counterbores, and tapped holes, all referenced to the bore that was just cut. The result is a cap whose pilot bore runs true to the housing: coaxiality within 0.015 mm, runout within 0.01 mm, and the hole pattern positioned within 0.02 mm.
Fits are held at IT6 to IT7 (H7/f7 class, about ±0.01 mm on the fitted diameters), and mating faces and the bore finish at Ra 0.8 um so seals and bearings seat without fuss.
Finishing is a fine bead blast followed by a silver clear anodize of 8 to 15 um: even, corrosion resistant, and pleasant to look at on an exposed joint. Marking is laser etched or ink jetted for traceability, and every lot is checked on CMM for bore coaxiality and hole position, with thread gauges and a micrometer closing the loop.
This part family supports the Robotics Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Pilot bore coaxiality within 0.015 mm and runout within 0.01 mm for true running end caps
- Hole pattern position within 0.02 mm for clean bolt up to the housing
- IT6 to IT7 fitted diameters (H7/f7 class, about ±0.01 mm), Ra 0.8 um on mating faces
- Fine bead blast plus silver anodize, 8 to 15 um film, corrosion and wear resistant
- Laser or ink jet marking for field traceability
- CMM, gauge, and roughness checks on every lot
Typical Applications
- End caps for servo and frameless motor housings
- Encoder mounts and covers on precision reducers
- Cylinder sealing caps for pneumatic and hydraulic actuators
- Joint cavity covers on humanoid and industrial robot arms
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
6061 or 7075 for an end cap?
6061-T6 covers most joint caps at lower cost and anodizes evenly. 7075-T6 earns its place where the cap carries structural load or the bolt pattern is dense. We quote either from the same route.
Will the anodize change my fitted dimensions?
Anodize grows the surface by roughly half the film thickness per face. We mask or pre-size fitted diameters so the final anodized part lands in your tolerance band, and the CMM report shows the as-delivered numbers.
Can you mark serials on each cap?
Yes, laser etching or ink jet marking per your format, applied after anodizing so it stays legible.
More Robotics & Humanoid Robots Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote