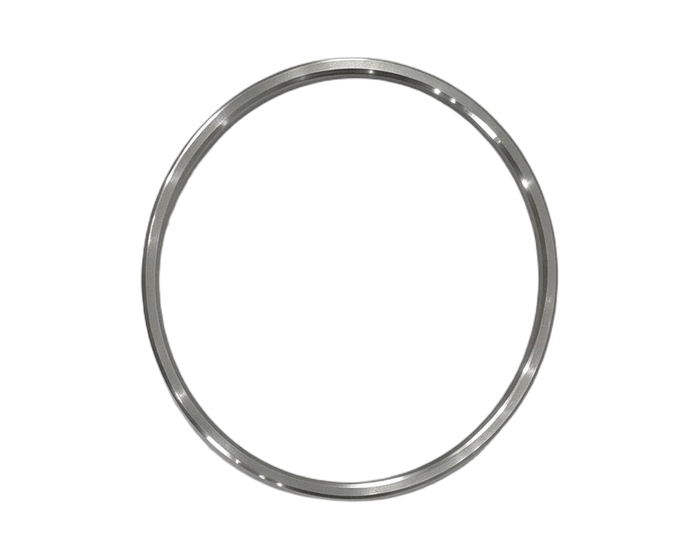
45 Steel Stator Retaining Ring, 73.9 mm OD, Flatness 0.02 mm, HRC 28 to 48
45 carbon steel motor stator retaining ring, 73.9 -0.10 mm OD by 69 +0.10 mm bore, 3 +/-0.03 mm thick, flatness 0.02 mm and parallelism 0.03 mm, quenched and tempered to HRC 28 to 48, precision ground faces, black oxide finish. Quote in 24 hours.
Semiconductor & Optics
A hardened 45 steel ring that clamps an 85 frame motor stator in place: precision ground 0.02 mm flat faces, 3 +/-0.03 mm thickness, quench and temper heat treatment, and a black oxide coat with rust preventive oil.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | 45 carbon steel (high quality structural) |
| Outside diameter | 73.9 -0.10 mm |
| Bore | 69 +0.10 mm |
| Thickness | 3 +/-0.03 mm |
| Flatness | 0.02 mm |
| Parallelism | 0.03 mm to datum A |
| Hardness | HRC 28 to 48, quenched and tempered |
| Edges | 4x C0.3, 0.5 x 45 degree breakouts |
| Finish | Black oxide with rust preventive oil |
| Process | CNC turning of ID and OD, precision face grinding, chamfer and deburr, quench and temper heat treatment, black oxide and oil |
| Inspection | Micrometer on thickness and diameters, flatness and parallelism checking fixtures, Rockwell hardness test |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
This thin ring presses against a motor stator to hold it in its housing, and its two dimensions carry the whole job. The bore at 69 +0.10 mm drops over the stator; the outside at 73.9 -0.10 mm registers in the housing; and the thickness at 3 +/-0.03 mm sets the clamp position. Flatness is held to 0.02 mm and parallelism to 0.03 mm, because a ring that rocks clamps the lamination stack unevenly and the assembly runs out of true.
The material route is what separates this from a soft spacer. 45 carbon steel is quenched and tempered to HRC 28 through 48, giving the ring the hardness to hold its clamp and resist wear over the motor's life. Heat treatment distorts, so the faces are precision ground after treatment, which is how a 3 mm ring reaches 0.02 mm flat. Edges carry C0.3 and 0.5 x 45 degree breakouts per the drawing.
Finish is functional: black oxide conversion with rust preventive oil, a dual defense that protects the steel through storage and assembly without adding measurable film to the precision faces. Appearance matters too, since the sheet calls for zero scratches or dents on this critical part; rings are handled and packed individually.
Verification matches the geometry: micrometer on thickness and diameters, dedicated flatness and parallelism checking fixtures, and Rockwell hardness sampling to confirm the heat treatment landed in the HRC 28 to 48 band.
This part family supports the Optical / Semiconductor Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- 45 carbon steel quenched and tempered to HRC 28 to 48
- 73.9 -0.10 mm OD by 69 +0.10 mm bore, 3 +/-0.03 mm thick
- Flatness 0.02 mm and parallelism 0.03 mm, ground after heat treatment
- Black oxide plus rust preventive oil for dual corrosion defense
- Edge breakouts C0.3 and 0.5 x 45 degree per drawing
- Handled and packed to a zero scratch appearance standard
Typical Applications
- 85 frame motor stator clamp and locating rings
- Press rings for motor assembly and stator retention
- Sealing and clamping washers in hardened carbon steel
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
| Lead Time | Prototypes 7 to 15 days; production scheduled by volume |
Common Questions
Why grind the faces instead of just turning them?
Heat treatment moves the part, and a turned face will not survive quench and temper at 0.02 mm flatness. Grinding after treatment is what gets the faces flat and parallel, which is the whole point of a clamp ring.
Why is hardness a range, not a number?
HRC 28 to 48 is the drawing's heat treatment window, tough enough to resist wear without going glass brittle. Every batch is verified with Rockwell testing to confirm the treatment landed in band.
What tolerances can you hold on rings like this?
The drawing's own callouts govern. Send the tolerance band together with the housing and stator interfaces, and we will confirm feature by feature what can be held before quoting.
More Semiconductor & Optics Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Semiconductor & Optics
Custom CNC Precision Machining Semiconductors Packaging Inspection Equipment and Automation Parts
View product →
Semiconductor & Optics
Microscope Quad Lens Seals for Medical and Laboratory Use
View product →
Semiconductor & Optics
OEM Custom CNC Precision Machining Semiconductors and Automation Part
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote