EGW Microscope Lens Barrel Mount in 6061, Turn Mill and 5 Axis Machined
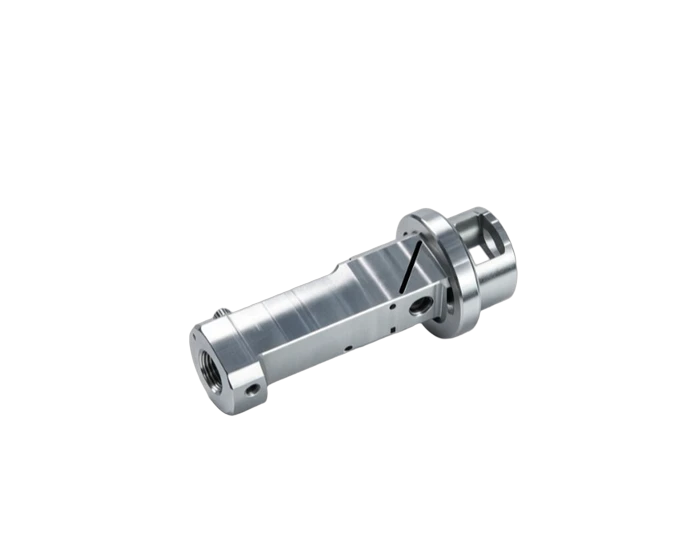
EGW lens barrel mount in 6061 aluminum: Ø10 mm optical bore at +0.05/0, coaxiality 0.03 mm, 45 degree slot at +/-0.5 degrees, M1.6 and M2 threads re tapped after anodize. Quote in 24 hours.
Semiconductor & Optics
Compact 22 by 18 by 63.5 mm barrel mount for precision microscopy and endoscopic imaging. One setup turn milling keeps the optical bore, flange, and 45 degree side slot in strict relative position.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Aluminum 6061 |
| Process | Turn mill center one setup turning of flange and bore, 5 axis milling of rectangular frame and 45 degree slot, thread protection and re tapping, 60 grit bead blast, matte anodize |
| Dimensions | 22 x 18 x 63.5 mm |
| Optical bore | Ø10.0 +0.05/0 mm, stepped seat Ø11.75 -0.05/0 mm |
| Coaxiality | Ø0.03 mm to datum A |
| Angle slot | 45 degrees +/-0.5 degrees, 1.0 mm wide, 2.5 mm deep |
| Threads | M1.6 and M2, re tapped after finishing |
| Finish | 60 grit glass bead blast, matte anodized |
| Inspection | CMM on coaxiality and slot angle, thread plug gauges 100 percent, microscope on bore edges |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
This mount sits at the front of an imaging chain, so its geometry is optical geometry: the Ø10.0 mm +0.05/0 mm light path bore runs the full length and must stay concentric with the Ø11.75 mm stepped seat within 0.03 mm, or the image drifts. The whole part is 22 by 18 by 63.5 mm.
The body is asymmetric by design: a cylindrical flange interface on one end, a rectangular lens group槽 slot on the other, and a 45 degree plus or minus 0.5 degree side slot, 1.0 mm wide and 2.5 mm deep, for an angled light path or locator. M1.6 and M2 threads on the side walls lock the optics in place.
Because the M1.6 and M2 threads would clog during bead blast and anodize, they are protected before finishing and precision re tapped after, per the drawing note. The 45 degree slot and the bore are cut in one multi axis setup to hold their relative position. Inspection uses CMM for coaxiality and slot angle, thread plug gauges on every M1.6 and M2, and a microscope check on the blast media and bore edges.
This part family supports the Optical / Semiconductor Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Ø10.0 mm +0.05/0 optical bore, coaxiality 0.03 mm to stepped seat
- 45 degree slot at plus or minus 0.5 degrees, 1.0 mm wide, 2.5 mm deep
- M1.6 and M2 threads re tapped after blast and anodize, no clogging
- Turn mill one setup geometry for bore to flange alignment
- 60 grit bead blast with matte anti reflection anodize
Typical Applications
- Lens barrel mounts for precision microscopes and endoscopic imaging
- Optical subassembly mounts with angled light paths
- EGW instrument optical carriers
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
| Lead Time | Prototypes 7 to 15 days; production scheduled by volume |
Common Questions
Why re tap M1.6 threads after anodize?
Blast media and oxide pack out tiny threads and ruin the class of fit. The drawing calls for protection before finishing and a second precision tap after, so every screw runs clean.
How is the 45 degree slot held to the bore?
Both features are cut in the same multi axis setup, so the position between them never sees a refixture. CMM verifies the angle and the relative position.
More Semiconductor & Optics Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Semiconductor & Optics
Custom CNC Precision Machining Semiconductors Packaging Inspection Equipment and Automation Parts
View product →
Semiconductor & Optics
Microscope Quad Lens Seals for Medical and Laboratory Use
View product →
Semiconductor & Optics
OEM Custom CNC Precision Machining Semiconductors and Automation Part
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote