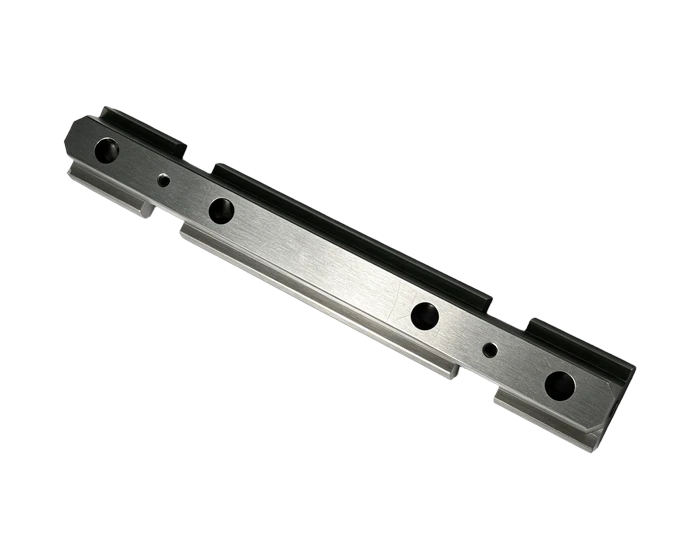
Large T-Slot Positioning Block in Prehard 4140 PH Steel, Ground and Nitrided
T-slot positioning block in prehard 4140 PH steel: parallelism and flatness 0.01, ground faces, plasma nitrided, demagnetized, inch tolerance control. Quote in 24 hours, no MOQ.
Semiconductor & Optics
A T-slot positioning block machined from prehard P20 (4140 PH grade) alloy steel: CNC roughing and finishing with surface grinding for the faces and steps, parallelism and flatness at 0.01, plasma nitrided for wear life and demagnetized before packing.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Prehard alloy steel, P20 plate stock HRC 28-34 (4140 PH grade) |
| Process | CNC roughing 0.1 mm stock, surface grinding of faces and steps, CNC finishing of profile and chamfers, tapping and counterboring, deburring, demagnetizing, plasma nitriding, anti rust oil |
| Form tolerances | Parallelism 0.01, flatness 0.01, profile 0.01 |
| Surface treatment | Plasma nitride, ground faces |
| Chamfers | 0.015 x 45 degrees where unspecified, all sharp edges removed |
| Tolerance system | Inch based drawing with decimal band control |
| Inspection | Dimensional check, burr and appearance check, demagnetization verified |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Positioning blocks live on machine tables and fixture plates where every micron of error repeats into the workpiece. This block is cut from P20 prehard plate at HRC 28 to 34, the 4140 PH class of alloy steel, so no post hardening distortion threatens the finished geometry.
The route runs CNC roughing with 0.1 mm stock per side, then a grinding operation that brings the four faces and steps to size, because grinding is what holds parallelism and flatness at 0.01. Finish milling then takes the profile, length, and chamfers, and the thread and counterbore features are completed on the mill. Inch based tolerances govern the drawing, with decimal band control on the precision features.
Plasma nitriding follows machining, hardening the surface for wear without changing the core or the dimensions. Before packing, every block is demagnetized, since a magnetized fixture block picks up chips and contaminates the next setup on the customer table. Edges are broken to 0.015 by 45 degrees and all sharp edges are removed.
This part family supports the Semiconductor Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Prehard P20 (4140 PH grade) plate, HRC 28-34, no post hardening distortion
- Parallelism and flatness 0.01 with profile accuracy 0.01
- Ground faces and steps, milled profile and chamfers
- Plasma nitride surface for wear resistance
- Demagnetized before packing to keep customer setups clean
- Inch tolerance band control, 0.015 x 45 degree default chamfers
Typical Applications
- T-slot positioning blocks on machine tables and fixtures
- Location datums in semiconductor precision drive assemblies
- Wear surfaces in clamping and locating fixture systems
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
Why prehard stock instead of hardening after machining?
Heat treating a finished block distorts it, and regrinding after that erases the economics. Prehard plate at HRC 28-34 machines cleanly and holds the ground geometry without a heat treatment step in the critical path.
What does plasma nitriding change on the dimensions?
It is a diffusion treatment, not a coating, so dimensional change is negligible. The block comes back to size, which is why nitriding can sit at the end of the route.
Why demagnetize a fixture block?
Machining and grinding leave residual magnetism, and a magnetized block holds fine chips against its locating faces. That contaminates the very surfaces the 0.01 flatness is for, so we verify demagnetization before packing.
More Semiconductor & Optics Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Semiconductor & Optics
Custom CNC Precision Machining Semiconductors Packaging Inspection Equipment and Automation Parts
View product →
Semiconductor & Optics
Microscope Quad Lens Seals for Medical and Laboratory Use
View product →
Semiconductor & Optics
OEM Custom CNC Precision Machining Semiconductors and Automation Part
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote