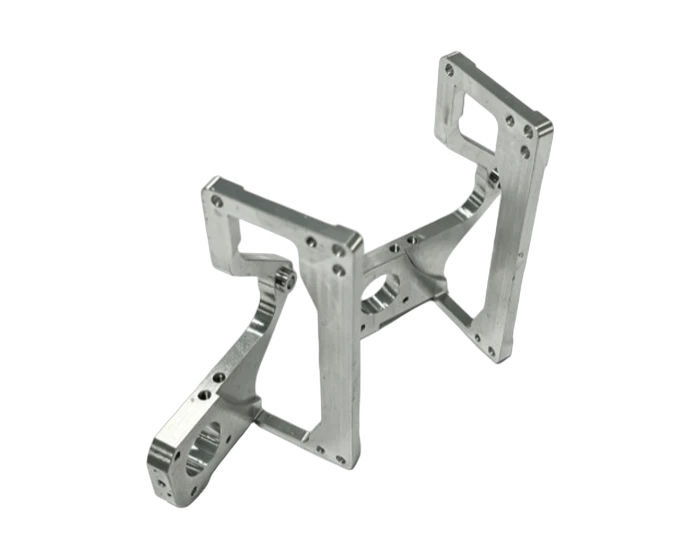
Precision Actuator Joint Structure Bracket, 5 Axis CNC Milled
5 axis milled actuator joint bracket in 7075/6061 aluminum: bearing bores 18.0 H7, parallelism and perpendicularity 0.02, Helicoil M2/M3 inserts, CMM 100 percent. Quote in 24 hours.
Semiconductor & Optics
A skeletonized thin wall bracket for actuator joints, 5 axis milled in 7075 or 6061 aluminum with motor flange faces, 18.0 H7 bearing bores, and M2/M3 Helicoil reinforced threads, checked 100 percent on CMM.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Aluminum AL7075-T6 or AL6061-T6, plate or bar stock |
| Process | 5 axis CNC milling in one setup, finish milling of flanges and bearing seats, drilling and tapping with Helicoil pre holes, insert fitting, micro deburring, ultrasonic cleaning |
| Locating bores | 18.0 H7 (+0.018/0) mm |
| Form tolerances | Parallelism and perpendicularity 0.02 A-B-C |
| Hole position | Cross face threaded pattern within 0.03 mm |
| Thread inserts | M2 / M3 Helicoil (wire thread inserts) |
| Inspection | CMM 100 percent on position and form, thread plug gauges, air gauge on bores |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Actuator joints want stiffness without mass, and this bracket is the answer in metal: large weight relief pockets with ribbed walls, motor mount flanges, bearing seat bores, and threaded holes protected by wire thread inserts. The part is milled in one 5 axis setup so the flange faces, bores, and pocket geometry all refer to one datum system.
Bearing and motor locating bores are held at 18.0 H7 (+0.018/0) mm, and parallelism and perpendicularity across the mounting faces hold at 0.02 against datums A, B, and C. Cross face position of the threaded hole pattern stays within 0.03 mm, tight enough that assembly needs no shimming. M2 and M3 holes are pre drilled at Helicoil insert depth so the aluminum threads strip proof, the inserts carry the load.
Thin walls over deep pockets chatter if you push the feed, so the roughing leaves stock and the finishing passes run at higher speed with short engagement. Left hand and right hand mirror versions are machined from the same program family with symmetry verified on CMM. Every piece is deburred at micron level, ultrasonic cleaned, and 100 percent checked for position and form, with thread gauges and an air gauge supporting the bore work.
This part family supports the Semiconductor Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- Skeletonized thin wall structure with ribs for high stiffness to weight ratio
- Motor and bearing locating bores at 18.0 H7 (+0.018/0) mm
- Parallelism and perpendicularity 0.02 across faces against A-B-C datums
- M2 / M3 Helicoil insert ready holes for strip resistant aluminum threads
- 5 axis single setup milling for cross face position within 0.03 mm
- Mirror left and right hand versions from one program family, CMM verified
Typical Applications
- Actuator joint structure brackets in precision mechanisms
- Motor and gearbox mounting frames in automation equipment
- Lightweight structural brackets for precision instrument assemblies
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
Common Questions
7075 or 6061 for this bracket?
Both are in the drawing. 7075 carries the higher load paths around the bearing seat, 6061 is the choice where weldability or cost matters more. We machine either to the same tolerances.
Why Helicoil inserts in an aluminum part?
Aluminum threads wear out first at the fastener. The stainless insert doubles the pull out strength and lets you service the joint repeatedly without losing clamp. We drill the pre hole depth and fit the inserts in house.
Can you keep thin walls from distorting after machining?
The pockets are cut with stress balancing passes and the walls are finished last with light engagement. Parts are measured after cooling, and if your assembly needs a post aging stabilization cycle we can add it to the route.
More Semiconductor & Optics Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Semiconductor & Optics
Custom CNC Precision Machining Semiconductors Packaging Inspection Equipment and Automation Parts
View product →
Semiconductor & Optics
Microscope Quad Lens Seals for Medical and Laboratory Use
View product →
Semiconductor & Optics
OEM Custom CNC Precision Machining Semiconductors and Automation Part
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote