Black Anodized Optical Lens Barrel in 6061/7075, Turn-Milled Stepped Bore, Matte Black Finish
Black anodized optical lens barrel, 60 to 90 mm diameter by 150 to 220 mm long, H6/H7 lens seats at +0.012/0 mm, 6H/6g fine optic threads, face runout within 0.01 mm and thread array coaxiality 0.015 mm, matte black anti reflection interior. Quote in 24 hours.
Semiconductor & Optics
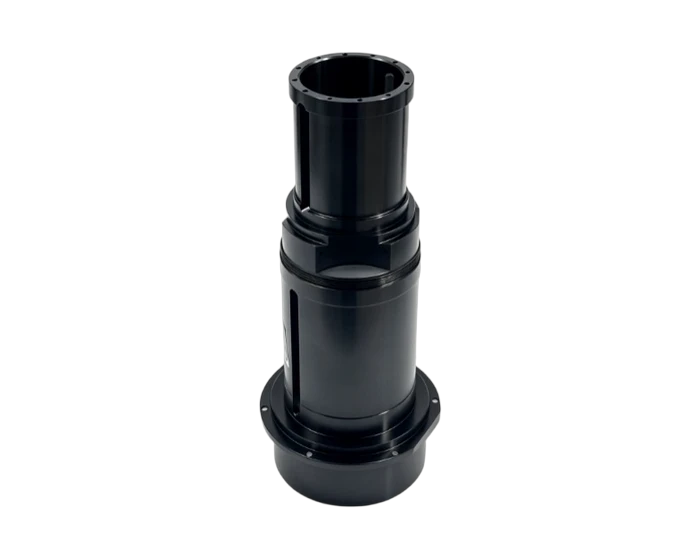
A multi stage optical lens barrel in black anodized aluminum: H6/H7 lens seats stacked down the bore, fine 6H/6g threads for retaining rings, an axial focus slot and a matte black interior that kills stray reflections.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | Aluminum 6061-T6 / 7075-T6 |
| Max outside diameter | Approx. 60 to 90 mm |
| Overall length | Approx. 150 to 220 mm |
| Lens seats | H6 / H7 internal steps, +0.012/0 mm |
| Threads | 6H/6g fine optic threads, external and internal |
| Face runout | 0.01 mm max |
| Coaxiality | 0.015 mm max on thread and seat array |
| Finish | Matte black anodized, anti reflective interior |
| Features | Seal grooves, diameter steps, end face tapped hole array, axial adjustment slot |
| Process | Tube or bar stock, turn-mill machining of bore steps, OD steps and threads in one setup, milling of end holes and axial slot, deburr, black anodize |
| Inspection | CMM on seat coaxiality, squareness and geometry; thread plug and ring gauges on 6H/6g threads; bore gauge on internal seats; reflectivity and coating uniformity check |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
This barrel holds a stack of lenses in alignment, which means every feature serves the optical axis. The internal bore steps down through several H6/H7 seats at +0.012/0 mm, each one landing a lens or spacer at its designed axial position, and each seat face running square to the axis so the lens does not tilt. Misalign a seat and the optics go soft; so the whole internal profile is bored in one chucking on a turn-mill center, keeping seat-to-seat coaxiality within 0.01 mm and the thread array within 0.015 mm.
The outside carries its own function: fine straight threads for focus and lens retaining rings, cut to 6H/6g optic grade so they turn smoothly without play, seal grooves, and diameter steps where mating hardware mounts. End faces carry arrays of small tapped holes for front hardware, and a precision axial slot machined down the sidewall gives access for focus adjustment or an aperture stop.
Thin walls and deep slots make the barrel delicate to machine. Cutting pressure on a thin section moves the part, and a moved part reads as out-of-round seats. The route stages roughing and finishing with stress relief between, uses sharp tooling with light finishing passes, and clamps on generous soft jaws so the final cuts come off a part that has already relaxed.
Finishing is matte black anodize, and it has two jobs here. Outside it is a hard, scratch resistant surface. Inside it is optical: the matte black, non reflective bore wall absorbs stray light that would otherwise scatter between lens elements. Film thickness is controlled so the precision seats and threads stay within their bands, and finished barrels are gauged with thread plug and ring gauges, bored seats checked with bore gauges, and the whole geometry re-verified on the CMM.
This part family supports the Optical / Semiconductor Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- H6/H7 lens seats at +0.012/0 mm bored in one chucking for axis alignment
- 6H/6g fine optic threads for smooth, backlash free focus and retaining rings
- Face runout within 0.01 mm, thread array coaxiality within 0.015 mm
- Precision axial sidewall slot for focus and aperture adjustment
- Matte black anti reflection anodize inside, hard black anodize outside
- Thread plug/ring gauges, bore gauges and CMM verification on every part
Typical Applications
- Lens barrels for optical instruments and imaging modules
- Opto mechanical housings in semiconductor inspection optics
- Multi stage aluminum barrels with fine threads and precision internal seats
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
| Lead Time | Prototypes 7 to 15 days; production scheduled by volume |
Common Questions
Why one chucking for the whole internal profile?
Because optical alignment is relative. Each seat only matters in relation to the others and to the threads. Turn the bore, flip the part and turn the rest, and you add a setup error between them that no amount of inspection removes. One chucking on the turn-mill keeps every seat and thread on the same axis.
How does anodizing stay off the precision sizes?
Film thickness is specified and the pre-plate dimensions are compensated for growth, the same discipline as any precision coated part. After coating, threads are gauged and seats re-measured, so the barrel that ships is verified in its finished state.
Why a matte black interior instead of plain anodize?
Stray light is the enemy inside a lens barrel. The matte black bore wall absorbs reflections that would otherwise bounce between elements and wash out contrast. It is an optical function, not cosmetics.
What tolerances can you hold on new lens barrels?
The drawing's own callouts govern. Send the tolerance band with the lens stack design, and we will confirm seat by seat what can be held after coating, before quoting.
More Semiconductor & Optics Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Semiconductor & Optics
Custom CNC Precision Machining Semiconductors Packaging Inspection Equipment and Automation Parts
View product →
Semiconductor & Optics
Microscope Quad Lens Seals for Medical and Laboratory Use
View product →
Semiconductor & Optics
OEM Custom CNC Precision Machining Semiconductors and Automation Part
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote