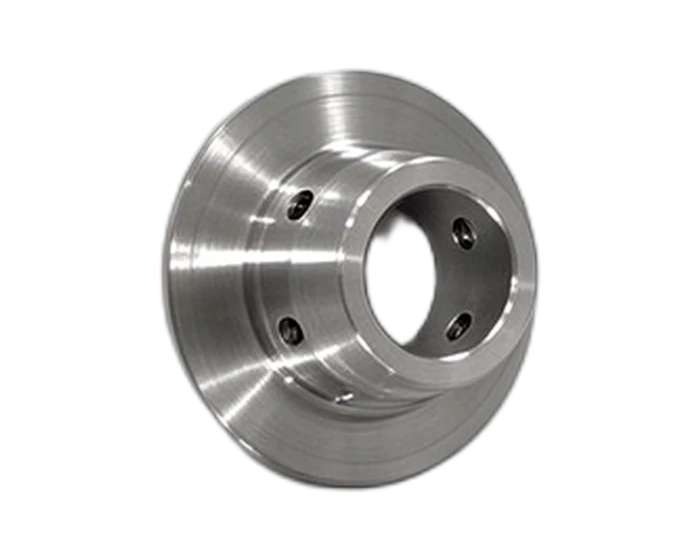
SUS304 Stainless Magnet Ring Seat, Turn-Mill Machined with Brushed Finish, 6x M3 Pattern
SUS304 hollow magnet ring seat, 32.5 g8 OD by 20 h7 bore with stepped 12.5 +/-0.01 mm bore, stacked heights 14.15 to 6.5 mm, coaxiality 0.02 mm to datum A, 6x M3 equally spaced, brushed corrosion resistant finish. Quote in 24 hours.
Semiconductor & Optics
A stainless ring seat that locates a motor magnet ring: g8 and h7 stepped fits down a 20 mm bore, one bore at 12.5 +/-0.01 mm, coaxiality 0.02 mm, and six M3 holes equally spaced on the flange.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | SUS304 stainless steel (06Cr19Ni10) |
| Outside diameter | 32.5 g8 |
| Main bore | 20 h7 |
| Stepped bores | 19 +/-0.05, 17 h6, 15 g8, 14.5 h7, 12.5 +/-0.01 mm |
| Heights | 14.15 +/-0.05, 12.4 +/-0.02, 7.5 +/-0.03, 6.5 +/-0.05 mm |
| Threads | 6x M3 equally spaced |
| Coaxiality | 0.02 mm to datum A |
| Finish | Brushed |
| Process | Turn-mill machining of full stepped profile, drill and tap of M3 pattern, deburr and edge dulling, brushing |
| Inspection | Caliper and micrometer on fits, thread plug gauges, coaxiality checking fixture with CMM sampling |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
This seat holds a motor's magnet ring concentric with the shaft, and its drawing says so with fits. The 32.5 g8 outside locates in the housing; the 20 h7 bore receives the magnet ring; and the stepped internal profile runs through 19 +/-0.05, 17 h6, 15 g8 and 14.5 h7 diameters down to a 12.5 +/-0.01 mm bore. Each of those letters is a controlled clearance or transition fit, the difference between a magnet ring that spins true and one that runs a tenth off and shakes the motor.
Heights are toleranced just as tightly because the seat stacks against shoulders: 14.15 +/-0.05, 12.4 +/-0.02, 7.5 +/-0.03 and 6.5 +/-0.05 mm. Coaxiality is held within 0.02 mm to datum A. The flange carries six M3 holes equally spaced for fastening.
Parts like this are the natural territory of a turn-mill center: the whole stepped profile, inside and out, is turned in one chucking so the fits share one axis, then the M3 pattern is drilled and tapped in the same setup chain. SUS304 is gummy and work hardens, so cutting is continuous with sharp tooling; dwelling skims and hardens the surface and the next pass pays for it. Every edge is deburred and dulled per drawing, since this seat is handled during motor assembly.
The finish is a brushed texture on the corrosion resistant 304 body. Verification runs caliper and micrometer across the fits, thread plug gauges in every M3, and CMM sampling on coaxiality and the stepped bore profile.
This part family supports the Optical / Semiconductor Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- SUS304 stainless with brushed corrosion resistant finish
- 32.5 g8 OD locating fit and 20 h7 magnet ring bore
- Stepped bores to 12.5 +/-0.01 mm with h6/h7/g8 controlled fits
- Stacked heights 14.15 +/-0.05, 12.4 +/-0.02, 7.5 +/-0.03, 6.5 +/-0.05 mm
- Coaxiality within 0.02 mm to datum A
- 6x M3 equally spaced, turn-milled in one setup chain
Typical Applications
- Motor magnet ring seats and covers in servo motor assemblies
- Concentric spacer seats in precision drive mechanisms
- Stainless stepped ring parts with controlled g8/h6/h7 fits
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 |
| Packaging | Individual bubble wrap, export carton or wooden case |
| Lead Time | Prototypes 7 to 15 days; production scheduled by volume |
Common Questions
Why so many different fits on one bore?
Each diameter does a different job. The g8 diameters are locating fits that slide, the h6/h7 bores locate precision parts with minimal play, and the +/-0.01 bore takes the tightest component in the stack. One seat, several mating parts, each with its own designed clearance.
How do you keep all the steps concentric?
They are turned in one chucking on the turn-mill center, so every step shares one setup axis, and coaxiality is verified to 0.02 mm against datum A rather than assumed.
What tolerances can you hold on new ring seats?
The drawing's own callouts govern. Send the tolerance band together with the mating housing and ring sizes, and we will confirm feature by feature what can be held before quoting.
More Semiconductor & Optics Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Semiconductor & Optics
Custom CNC Precision Machining Semiconductors Packaging Inspection Equipment and Automation Parts
View product →
Semiconductor & Optics
Microscope Quad Lens Seals for Medical and Laboratory Use
View product →
Semiconductor & Optics
OEM Custom CNC Precision Machining Semiconductors and Automation Part
View product →Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote