Fiber Optic Gyro IMU Shield Support in 1J79, Heat Treated and Certified
1J79 soft magnetic support bracket for fiber optic gyro IMUs: ISO 2768-mK, Ra 1.6, TTH heat treatment 4h at 1150 C certified, serial laser marking, 3.1 material certificate. Quote in 24 hours.
Aerospace
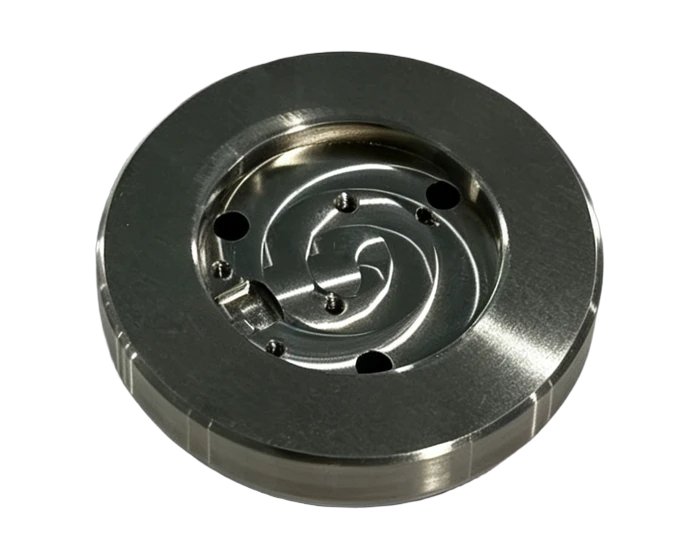
A magnetic shield support bracket for fiber optic gyro IMUs, machined from 1J79 (ASTM A753 Alloy 4) soft magnetic alloy, heat treated 4 hours at 1150 C with certificate, laser serialized, and shipped with first and last article reports and a 3.1 material certificate.
Or email drawings to kgl@kglmfc.com
Key Specifications
| Parameter | KGL Capability |
|---|---|
| Material | 1J79 soft magnetic alloy (UNS equivalent per ASTM A753 Alloy 4), bar stock |
| Process | Material verification; heat treatment TTH 4h 1150 C; wire EDM cutting; 4-axis CNC milling; CNC turning; CNC milling; surface grinding; deburring; cleaning and packing |
| General tolerance | ISO 2768-mK |
| Surface finish | Ra 1.6 um general |
| Unit weight | 46.84 g |
| Marking | Laser, ARIAL, 2 mm character height, in 19.5 x 7 mm drawing zone; serials increment per drawing range |
| Quality documents | First and last article dimensional report with bubble diagram, OK/NOK judgment, numbered labels; 3.1 material certificate; heat treatment certificate |
| Inspection | In process size and appearance checks; 100 percent final visual recheck |
| Tolerance | ±0.005 mm standard on metals, engineering plastics, and carbon fiber composite |
| Certifications | ISO 9001:2015, ISO 13485:2016, AS9100D |
| Capacity | 100+ CNC machines including 11 five-axis centers |
| MOQ | No MOQ; 1-piece prototypes supported |
| Quote | Within 24 hours for complete 2D/3D files |
About This Part
Inside a fiber optic gyro IMU, this bracket does two jobs at once: it holds the optical stack in position and it closes the magnetic shielding path, because 1J79 is a nickel iron soft magnetic alloy that conducts flux the way copper conducts current. Machining it wrong ruins both jobs, so the route is built around protecting the material's magnetic properties.
Bar stock is verified chemically, heat treated 4 hours at 1150 C (TTH cycle) with a certificate, then cut by wire EDM, turned, milled, and surface ground to ISO 2768-mK with Ra 1.6 general finish. Each part carries a serial laser mark in the drawing specified 19.5 by 7 mm zone, incrementing per the drawing range, at 2 mm ARIAL character height.
First and last article pieces of every batch get a full dimensional report with a bubble diagram and OK/NOK judgment on tagged labels, and 100 percent visual recheck closes the lot. Shipments include the 3.1 material certificate and heat treatment certificate in the tray pack.
This part family supports the Aerospace Parts industry. Read how KGL machines parts for that sector, then send your drawing for a quote.
Why Machine It at KGL
Five-Axis Fleet
100+ CNC machines including 11 five-axis centers run complex geometry in single setups, so tolerances do not stack up across refixturing.
Verified Accuracy
±0.005 mm standard on metals, plastics, and carbon fiber composite, verified on Hexagon and Zeiss CMMs (0.0015 mm accuracy).
Fast Prototypes
Engineering feedback with every quotation; prototype parts typically machined in 15 to 25 days.
One Supplier, End to End
Material sourcing, machining, heat treatment coordination, finishing, CMM inspection and export packaging under one roof.
Part-Specific Advantages
- 1J79 (ASTM A753 Alloy 4) nickel iron soft magnetic alloy for combined support and shielding
- Heat treatment TTH 4h at 1150 C, applied and certified to protect magnetic properties
- ISO 2768-mK general tolerance, Ra 1.6 general surface finish
- Serial laser marking per drawing zone (19.5 x 7 mm, ARIAL 2 mm), incrementing per range
- First and last article full dimension reports with bubble diagram and OK/NOK labels
- 3.1 material certificate and heat treatment certificate with every shipment
Typical Applications
- Magnetic shield support brackets inside FOG inertial measurement units
- Precision soft magnetic carriers for navigation and guidance sensors
- Instrumentation brackets needing combined structural and flux path function
Commercial Terms
| Commercial | Detail |
|---|---|
| MOQ | No MOQ; 1-piece prototype supported |
| Quote | Within 24 hours for complete 2D/3D files |
| Terms | EXW / FOB Shenzhen |
| Certifications | ISO 9001:2015 / AS9100D |
| Packaging | Tray pack with first and last article reports, bubble diagram, and 3.1 material certificate |
Common Questions
Why does heat treatment matter so much on 1J79?
The magnetic permeability of 1J79 depends on the heat treatment structure. The 1150 C cycle restores the soft magnetic properties after machining stress, and the certificate proves the cycle was actually run, not assumed.
What is a first and last article report?
The first and the last piece of the batch are measured against every drawing dimension, recorded on a bubble diagram with pass or fail judgment and numbered labels, so you can trace exactly what the lot contained at both ends.
Can you serialize beyond 150 pieces?
Yes, the marking format and increment range follow your drawing; the photographed lot ran the series called out there, and any range works the same way.
More Aerospace Parts
Other parts KGL machines in this industry. Every card links to its own detail page.
Ready to Machine This Part?
Send your 2D/3D drawings and get a quote within 24 hours. No MOQ for prototypes and small lots.
Request a Quote