CNC Machining for Optical Equipment
Lens barrels, adjustment mounts and precision carriers machined to the concentricity and surface quality optical assembly lines expect, with clean packing as standard.
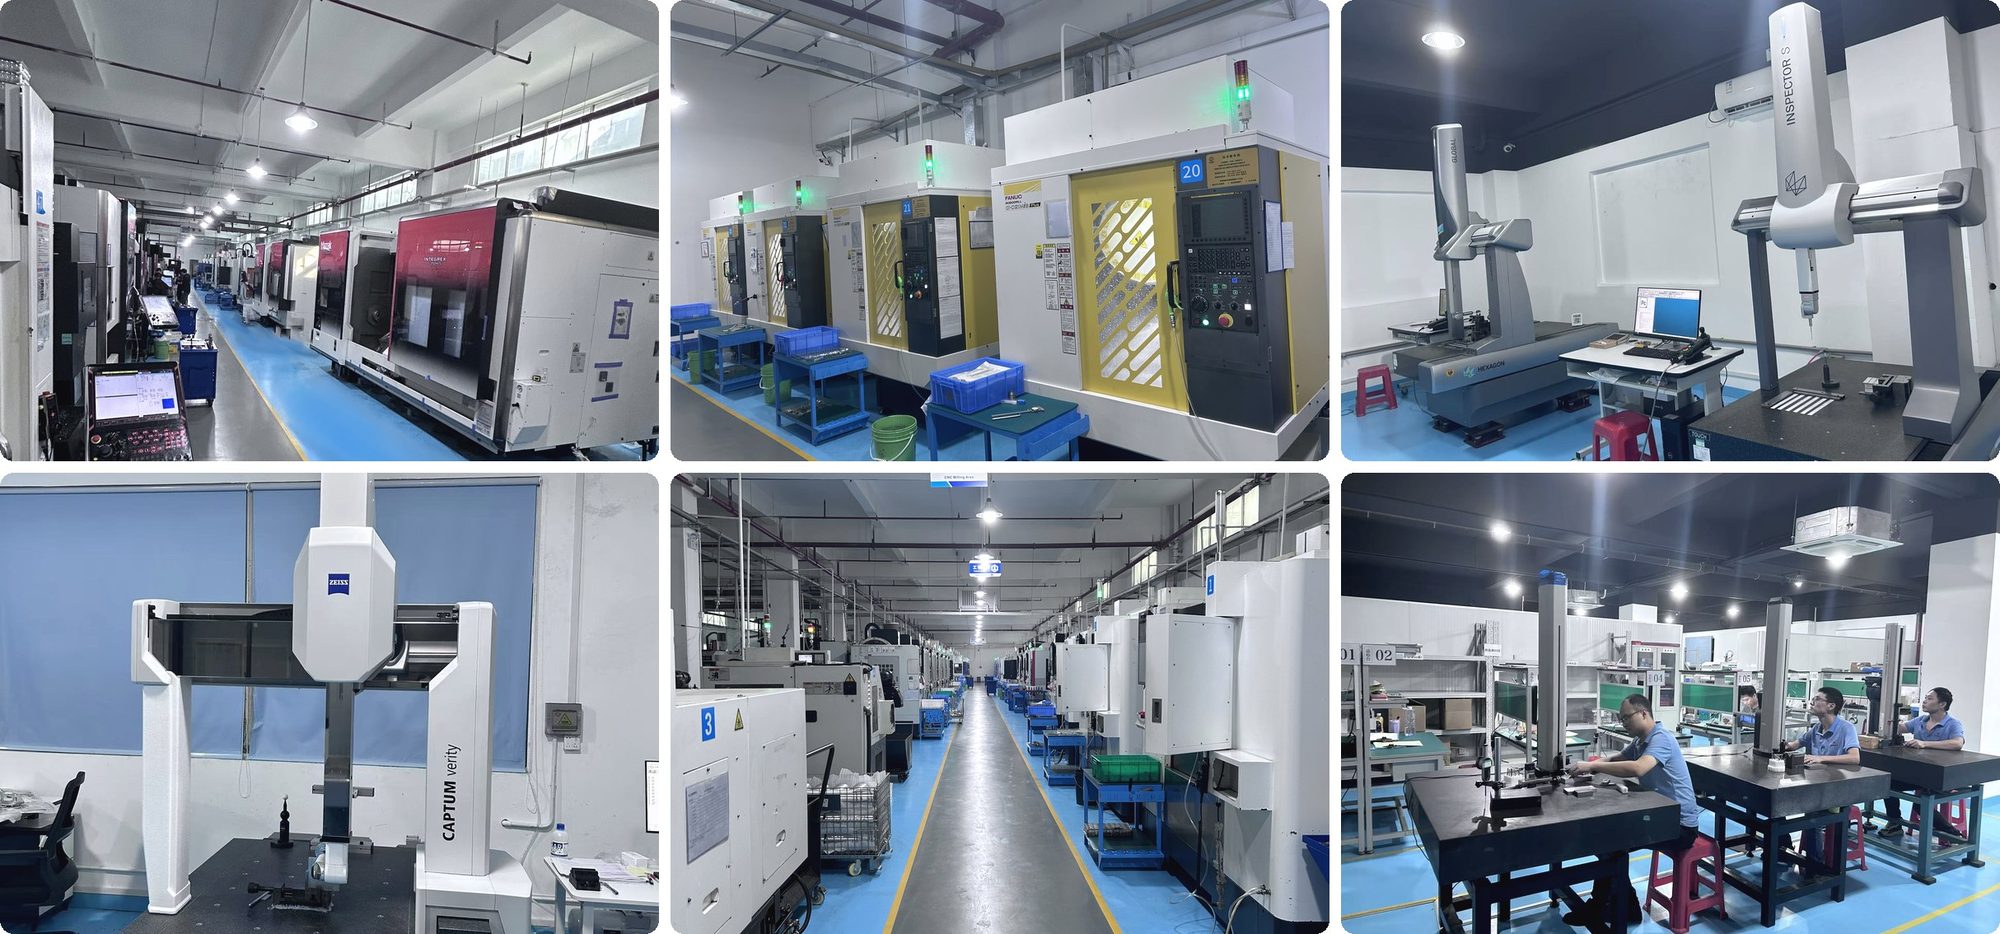
What We Build for Optical Teams
- Lens barrels with internal retainer threads, concentricity 0.005 mm
- Mirror and prism mounts with datum-defined pads, +/-0.005 mm feature-to-feature
- Adjustment mechanism bodies for alignment stages
- Camera and sensor carriers machined five sides complete
Optical Face Quality
| Feature | We hold |
|---|---|
| Bore concentricity | 0.005 mm typical |
| Bore surface | Ra 0.4 or better |
| Mount pads | Flatness 0.005 mm on seating faces |
| Cosmetic surfaces | Per agreed inspection sample, packed clean |
Related program: optical lens barrel case study. Typical parts: optical typical parts.
Optical Machining FAQ
What makes optical machining different?
Datum discipline and surface quality. Bores that hold lenses run concentric within 0.005 mm and Ra 0.4 or better, mounting faces stay stress-free, and parts are cleaned and packed so no particle reaches the assembly line.
Can you machine lens barrels with internal threads for retention rings?
Yes, internal threads and retainer grooves are cut on lathes with live tooling, gauge checked, with concentricity documented on the CMM report.
Do you handle small volume optics-adjacent parts?
Yes, prototype batches of 10 to 50 are common in this industry, and repeat batches keep the same fixtures and programs.
Machining Optics-Adjacent Parts?
Send the drawing; quote with concentricity and surface plan within 24 hours.
Request a Quote