CNC DFM Checklist: 15 Rules to Check Before You Send a Drawing
The fifteen design for manufacturability checks our quoting engineers apply to every incoming drawing, grouped by geometry, tolerances and datums, and material plus finish, with the cost each one removes.
Most machining cost is fixed before the machine ever runs, in the geometry, tolerance, and material decisions written on the drawing. That is why every RFQ that reaches our desk goes through the same DFM review before a number is attached: the quoting engineer and the process planner read the drawing against the list below, and anything that fights the process comes back to you with a reason and a cheaper alternative. This checklist is that review, written so you can run it yourself before you send the file.
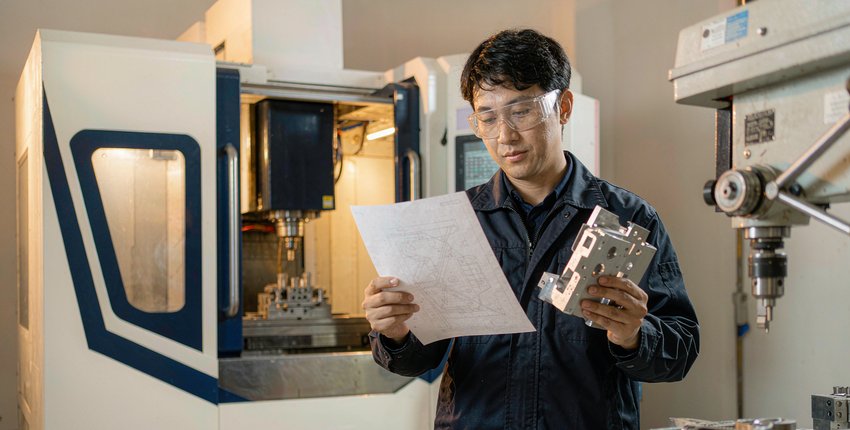
Rules 1 to 5: geometry
Geometry rules decide how many tools the job needs, how deep they reach, and how many setups the part demands. Five checks catch the expensive cases.
| Rule | The check | What ignoring it costs |
|---|---|---|
| 1. Pocket depth | Depth under 4 times the smallest tool diameter; deeper pockets opened with progressive passes | Long-reach tools, more passes, deflection and finish risk |
| 2. Internal corner radii | Radius at least a third of the pocket depth, and larger than the tool corner radius | Extra cutter sizes, hand finishing, visible mismatch |
| 3. Hole depth to diameter | Drilled holes under 5 diameters deep; deeper holes stepped or gun-drilled | Drill wander, broken tools, extra operations |
| 4. Wall thickness | Uniform walls; no heavy mass feeding a thin web; minimum 0.5 mm in aluminum, more in stainless | Distortion after machining, out-of-tolerance flatness |
| 5. Threads | Blind threads 1.5 to 2 times diameter engagement; bottom clearance for the tap; class stated | Broken taps, shallow engagement, rework |
The floor example that repeats most often is rule 2. A pocket 12 mm deep with a 1 mm corner radius forces a 2 mm cutter through the full depth; the same pocket with a 4 mm radius runs a 6 mm cutter at three times the removal rate. The radius change is free on the drawing and shows up immediately in the quote.
Rules 6 to 10: tolerances and datums
Tolerance placement decides how the part is measured, which decides cycle time and inspection cost. Five checks separate the functional callouts from the expensive ones.
| Rule | The check | What ignoring it costs |
|---|---|---|
| 6. Tight bands only where needed | Plus or minus 0.005 mm reserved for functional features; general block covers the rest | Every dimension measured and chased, cycle time climbs |
| 7. Machined datums | Datums reference machined surfaces, not cast or sawn faces | False readings, arguments about what the datum means |
| 8. One datum chain | Dimensions from one side of the part, not from both ends | Stacked error between features that must fit together |
| 9. Position over coordinate pairs | True position callouts for hole patterns that must align | Oversized or undersized zones for the real function |
| 10. Finish only on functional faces | Ra callouts on seals and seats, general note elsewhere | Finishing time multiplied across cosmetic faces |
Rules 6 and 10 are the same idea in two units: put the tight number only where the function needs it. Our tolerance chart shows what each band costs to hold, and the Ra chart maps finish values to the functions that need them. If a drawing carries GD&T frames, the GD&T guide explains how each callout will be measured.
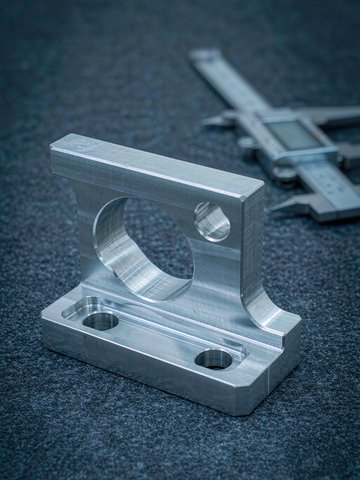
Rules 11 to 15: material, finish, and the RFQ itself
The last five checks cover what the part is made of, how it is coated, and what the buyer tells us about quantity and intent.
| Rule | The check | What ignoring it costs |
|---|---|---|
| 11. Full material callout | Grade and temper or condition, for example 7075-T651 or 17-4PH condition A | Wrong stock purchased, strength or corrosion mismatch |
| 12. Coating limits stated | Surfaces that stay bare, and finish measured before or after coating | Dimensions consumed by the coating, sealing faces plated over |
| 13. Environment noted | Salt, washdown, chemicals, or temperature where the part serves | Alloy and finish chosen for the wrong service |
| 14. Critical features marked | Drawing notes the features that need CMM or first-article layout | Inspection scope argued after production instead of priced |
| 15. Quantity bands | RFQ carries target quantity or a band, not a blank | Quote assumes a batch size that is not yours |
Rule 12 pairs with the finish comparison guide, because anodize and electroless nickel both grow the part and the drawing should state which faces are excluded. Rule 11 matters most on the materials library side of the quote: stocked grades move the day the order releases, while a callout without a temper sends the buyer back to the mill certificate.
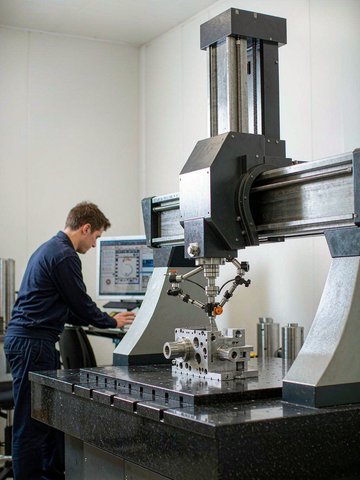
What happens after you send the drawing
Every RFQ through the quote form runs this checklist twice: once by the quoting engineer who prices the route, once by the process planner who will run it. When a rule is broken, the quote returns with a DFM note that names the issue and the alternative, so the change happens before the purchase order, not during production. Typical notes from the last quarter: a 1.5 mm radius opened to 3 mm to save a cutter, an Ra 0.8 callout moved off a cosmetic face, and a blind M3 thread shortened from 3 to 1.5 times engagement after the drawing could not explain the extra depth.
The wider cost context lives in the cost factors guide, and the same design choices appear in production stories on the blog, for example how design choices cut machining cost on real parts. If the drawing is still in motion, send the current revision anyway; the review works on the geometry, and the DFM notes carry over to the next revision at no charge.
Frequently asked questions
Do you return DFM notes with every quote?
When a drawing has a feature that fights the process, yes, the note names the issue and the alternative with the reason. Drawings that are already clean come back with a confirmation of the route instead of a lecture.
What is the most common DFM issue you see?
Internal corner radii sized for appearance rather than tooling, and tight tolerances spread across features that do not function together. Both are free to fix on the drawing and expensive to fix on the floor.
How much can DFM changes reduce the price?
On parts with a few fixable features, cycle time typically drops 10 to 25 percent, plus removed setup and inspection steps. The note tells you the specific number for your drawing rather than a blanket promise.
Can I send an incomplete drawing for DFM review?
Yes. Geometry without final tolerances still produces useful notes on radii, depths, and walls. Mark the open items and the review will flag what needs a decision before quoting can finish.
More Reference Guides
Charts and decision guides from the KGL engineering desk.
CNC Machining Tolerance Chart: IT Grades and What It Takes to Hold 0.005 mm
Read the reference →
Surface Roughness Ra Chart: What Ra 0.4 to Ra 3.2 Means and What Each Finish Costs
Read the reference →
5-Axis vs 3-Axis CNC Machining: Cost, Setups, and When the Upgrade Pays
Read the reference →
6061 vs 7075 vs Titanium: An Alloy Selection Guide for Machined Parts
Read the reference →
Anodizing vs Chem Film vs Electroless Nickel: Choosing a Finish for Machined Parts
Read the reference →
Stainless Steel 304 vs 316 vs 17-4PH: A Machining Perspective
Read the reference →
CNC Machining Cost Factors: What Actually Drives the Price
Read the reference →
GD&T Basics for Machined Parts: Datums, Position, and What Actually Gets Measured
Read the reference →
Tight-Tolerance Machining: The Five Steps Behind a 0.005 mm Result
Read the reference →Have a drawing to check?
Send it to kgl@kglmfc.com or request a quote. Engineering review responds within 24 hours.
Request a Quote